
Engineered Coil Processing Systems & Shearing Units
Explore our flagship heavy-duty lines, manufactured with in-house stress-relieved steel frames, hardened alloy tooling, and closed-loop Siemens CNC automation.

High Strength Leveling Machine
Engineered for high-yield AHSS coils up to 1200 MPa, eliminating coil set, crossbow, and localized residual stress through 4-Hi/6-Hi multi-roller clusters.
Configure Machine
Professional Straightening Machine
Micrometer-grade motorized gap adjustment for metal sheets and thick plate strips prior to laser cutting, deep stamping, and automated profile bending.
Technical Specs
Hot Rolled Plate Moving Shear Line
Synchronized servo rack-and-pinion carriage accelerates with continuous hot-rolled strip flow, cutting thick gauges up to 25mm without stopping the leveling line.
View Shearing Line
Stainless Steel Coil Uncoiling-Leveling-Shearing-Stacking Line
Zero-mar polyurethane rollers, synchronized protective PVC film laminators, and air-cushion drop stackers preserving pristine BA and No.4 mirror finishes.
Explore CTL System
HR Coil Uncoiling-Slitting-Leveling-CTL-Stacking Line
All-in-one footprint providing both high-speed longitudinal mult-slitting and transverse precision blanking, optimizing warehouse layout and ROI.
Review Layout
HR Sheet Uncoiling, Slitting & Recoiling Line
Equipped with twin slitter heads for rapid 15-minute off-line knife setups, hydraulic looping pit dampers, and variable back-tension bridle stands.
Explore Slitting Line
HR Uncoiling-Slitting-Recoiling Line
Heavy-gauge strip preparation for downstream HF welded tube mills and structural roll formers, operating reliably at line speeds up to 180 m/min.
Request Quotation
HR Sheet Uncoiling-Leveling-Shearing-Stacking Line
High-speed hydraulic guillotine or pneumatic shear coupled with optical length encoders, delivering diagonal sheet squareness under ±0.5mm/m.
Custom EngineeringGlobal Coil Processing & Shearing Systems Landscape
The international metal coil processing industry is undergoing a structural paradigm shift driven by high-yield materials, micro-burr tolerances, and automated digital production lines.
Surging Scrap Cost Economics
With raw hot-rolled and stainless master coil pricing experiencing sustained global volatility, slit edge trim waste and sheet length overruns directly erode operating margins. Modern precision rotary slitters and flying shears minimize edge scrap down to under 0.8% of gross tonnage.
Zero-Tolerance Stamping Demands
Automated robotic press lines in OEM EV factories reject steel sheets with internal residual stress that creates spring-back or bow during deep drawing. This has transformed multi-roll leveling machines from optional accessories into critical metallurgical conditioning engines.
High-Speed Continuous Shearing
Legacy start-stop stop-motion shears bottle-neck downstream logistics. Steel mills are replacing stationary guillotines with high-acceleration flying shears and rotary drum shears capable of cutting 3000mm sheets at line velocities exceeding 100 meters per minute.
The China Manufacturing Advantage: The Wuxi Metallurgical Hub
How Wuxi Jianfa combines deep regional supply chain density, vertically integrated heavy machining, and aggressive CAPEX efficiency to deliver tier-one performance globally.
100% In-House Heavy Machining & Annealing
Across our dedicated 40,000 m² factory footprint, machine frames, leveler bridges, and slitter arbor housings undergo proprietary thermal stress-relief annealing followed by single-setup processing on high-precision CNC floor-type boring mills and double-housing plano-milling centers.
Sub-50km Supply Chain Radius
Forged 42CrMo/GCr15 alloy roll blanks, induction hardening facilities, precision bearings, and Rexroth-certified hydraulic manifolds are sourced and verified within a 1-hour logistics perimeter, slashing equipment manufacturing lead times from 12 months down to 14–18 weeks.
40–60% Capital Expenditure Efficiency
Global buyers acquire European-benchmark metallurgical cutting and leveling tolerances (±0.05 mm slitting accuracy, <0.5 I-Unit flatness) while reducing line acquisition capital by up to 50%, dramatically compressing the payback curve for international service centers.
System Architecture: Slitting Lines vs. CTL Lines vs. Flying Shears
Comprehensive metallurgical breakdown of mechanical kinematics, tooling calculations, and continuous throughput vectors across the three core coil processing lines.
| Engineering Parameter | High-Precision Slitting Line | Stop-Start Cut to Length (CTL) Line | Continuous Flying Shear Line |
|---|---|---|---|
| Primary Finished Geometry | Multiple precision-slit narrow coil mults | Discrete rectangular sheets or shaped blanks | High-volume uniform stacked steel sheets |
| Cutting Mechanism & Kinematics | Rotary circular male/female knives with stripper rings | Hydraulic guillotine or mechanical eccentric shear | Rack-and-pinion synchronized moving shear / rotary drum |
| Strip Motion During Shearing | Continuous high-velocity web movement | Stationary pause via looping pit index or servo feed | 100% continuous speed without web deceleration |
| Leveling Integration | Optional 2-Hi/4-Hi strip flattener | Essential 4-Hi / 6-Hi precision roller leveler | Essential high-speed cassette roller leveler |
| Thickness Capability | 0.15 mm – 16.0 mm | 0.3 mm – 25.0 mm heavy plate | 0.4 mm – 12.0 mm medium gauge |
| Standard Line Speed | Up to 200 m/min | 30 – 60 m/min (limited by cycle stop) | 80 – 120 m/min continuous velocity |
| Tolerance Benchmarks | Width: ±0.03 mm; Burr: <3% t | Length: ±0.3 mm; Diagonal: ±0.5 mm | Length: ±0.5 mm @ 100 m/min |
Specialized Industrial Application Scenarios
Tailored configurations engineered to meet the unique surface, metallurgical, and dimensional criteria of premier global industries.
Automotive Stamping & Body-in-White
Dedicated cut-to-length and trapezoidal blanking lines processing exposed and unexposed automotive sheet (CR4, DP600/DP980). Features magnetic belt stackers and electrostatic wash-oiler integration to prevent abrasive particulate defects.
Electrical Steel & Transformer Cores
Ultra-high-precision slitting lines for cold-rolled grain-oriented (CRGO) and non-oriented (CRNGO) silicon steel. Incorporates carbide rotary knives mounted on dynamically balanced arbors runout-tested to within ≤0.003 mm to prevent core loss-inducing burrs.
Heavy Structural & Pipe Fabrication
Massive hot-rolled coil slitting configurations built for API-grade casing and ERW line pipe feedstocks up to 16 mm thickness. Features heavy hydraulic wedge peelers, four-roll rough straighteners, and dual scrap ballers/choppers.
Architectural Stainless & Aluminum
Mirror-finish processing utilizing full non-contact vacuum uncoiling systems, synchronous top/bottom PE protective film application, rubberized tension stands, and automated air-float stacking tables protecting against scratch hazards.
The Future: AI Automation, Closed-Loop Laser Metrology & Servo Electrification
Discover how intelligent cyber-physical systems are transforming traditional shearing hardware into autonomous, self-optimizing metallurgical manufacturing lines.
Automatic Knife Tooling Calculation
Integrated line software automatically calculates knife clearance, rubber stripper durometer selection, and shim spacing directly from tensile test inputs. Paired with robotic semi-automatic slitter tooling arms, changeovers drop from 90 minutes to under 8 minutes.
Closed-Loop Laser Surface Metrology
Continuous real-time laser triangulation scanning inspects sheet flatness, camber, and edge burrs dynamically at 100 m/min. The laser system transmits real-time micro-deflection signals to hydraulic leveler back-up rolls, neutralizing shape deviations instantly.
Full-Servo Shearing & Regenerative Power
Eliminating traditional hydraulic reservoirs in flying shears via ultra-responsive permanent magnet servo motors. Common DC bus architecture channels regenerative kinetic braking energy back into the line grid, slashing energy consumption by 28–35%.
Global Enterprise Procurement Evaluation Framework
A disciplined technical due diligence methodology for corporate procurement managers, plant directors, and CAPEX steering committees investing in heavy machinery.
1. Slitter Arbor Deflection Limits
Verify that slitter arbor shaft diameters are engineered with finite element analysis (FEA) to maintain static runout under 0.005 mm and dynamic deflection under 0.01 mm under maximum coil mult shear load. This parameter directly governs edge burr depth and blade longevity.
2. Tension Stand Configuration
Different strip gauges and surface finishes require specialized back-tension methodologies to eliminate loose coils during recoiling. Ensure your supplier provides combined roll-tension, pad-tension, and pneumatic belt bridle units tailored to delicate stainless or oiled HR steel.
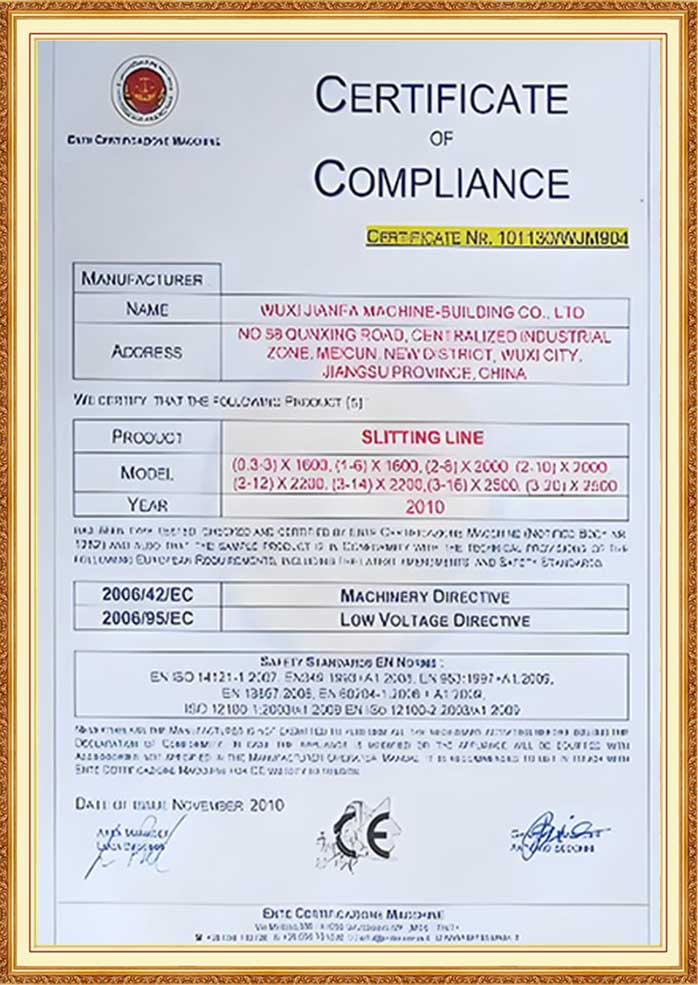
3. Safety Architecture (CE & EN Standards)
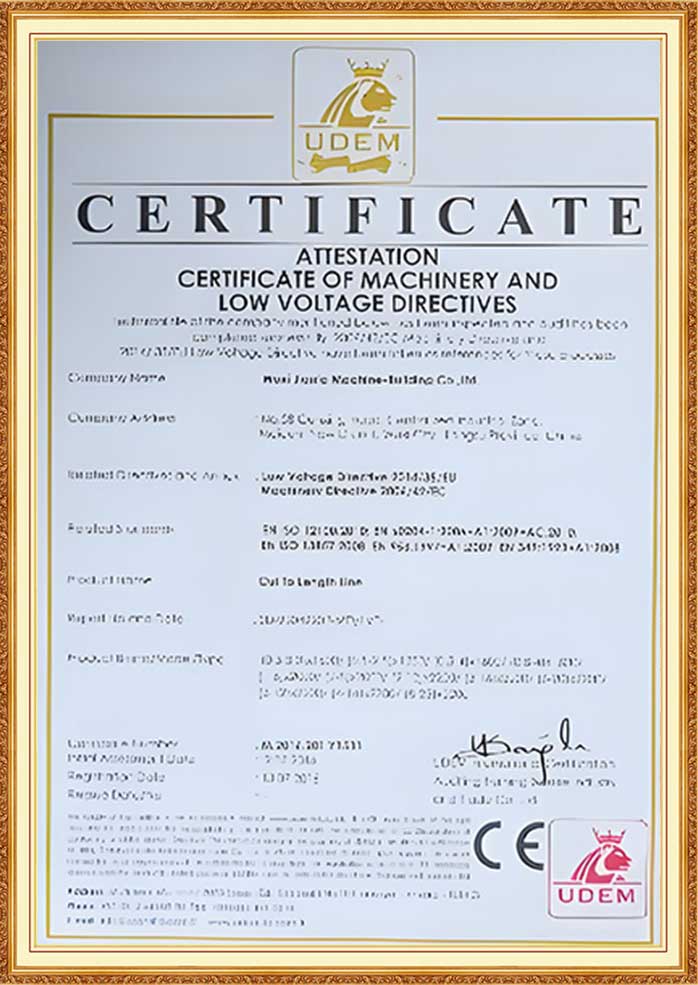
Confirm compliance with EN ISO 13849-1 functional safety category 3 or 4. Certified lines must include multi-beam safety light curtains around uncoilers and loop pits, keyed interlocks on knife enclosures, and hydraulic zero-energy deadband dump valves.
Global Footprint & Verified Enterprise Credentials
With machines running in over 30 countries across six continents, Wuxi Jianfa is recognized as a National Key Developing Enterprise in the metallurgical equipment industry.
- United States
- Mexico
- Brazil
- Argentina
- Germany
- Türkiye
- Russia
- Kazakhstan
- Egypt
- South Africa
- UAE
- India
- Vietnam
- Malaysia
- Indonesia
- Australia
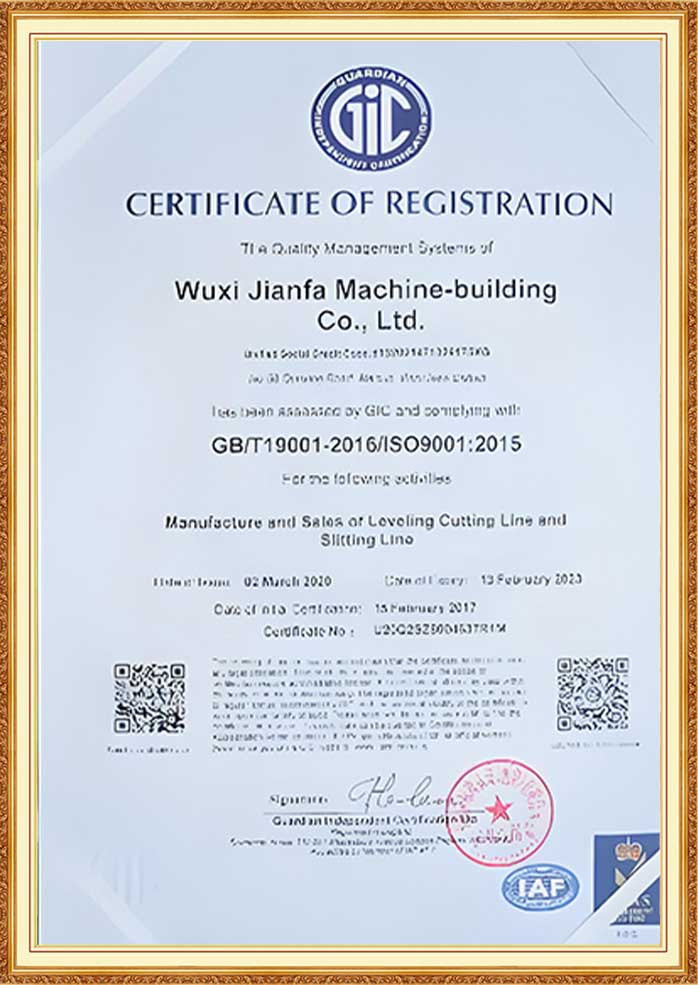
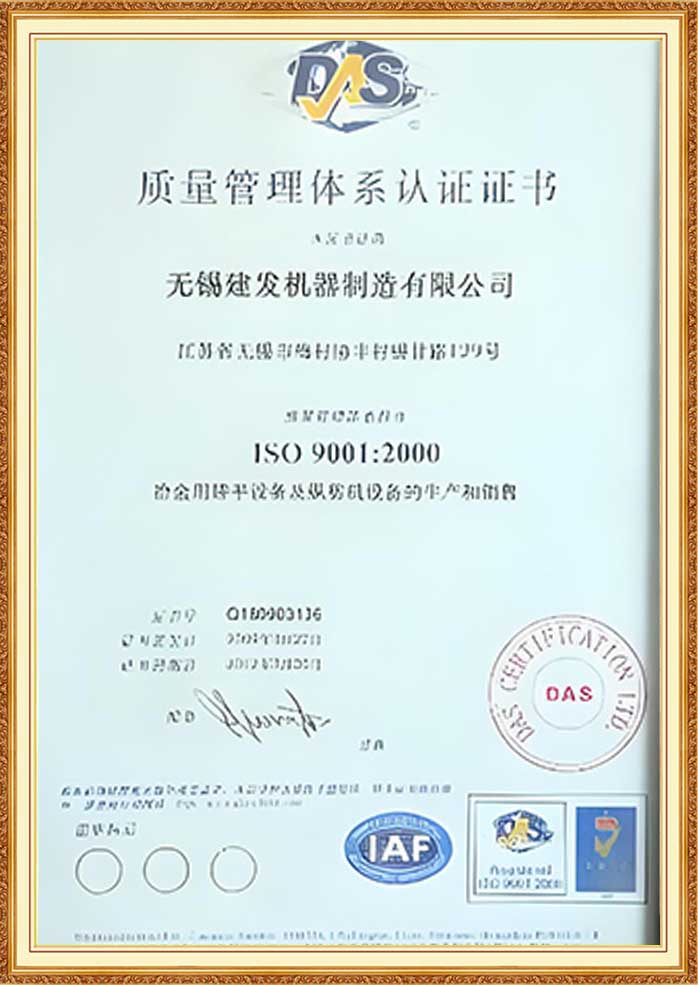
Official Enterprise Certifications & Industry Accreditations
Click on any documented qualification to verify full compliance records.
Frequently Asked Technical Questions (FAQ)
Direct, engineering-backed answers covering equipment sizing, steel metallurgy tolerances, tooling wear formulas, and international turnkey commissioning.
What coil processing equipment does Wuxi Jianfa Machine-Building specialize in?
What material grades, thicknesses, and yield strengths can your equipment process?
How do I choose between a Cut to Length Line (CTL) and a Flying Shear Line?
How is slitter knife clearance calculated to prevent excessive edge burr?
What foundation and power infrastructure is required before installation?
How are surface-sensitive materials like mirror stainless or automotive skin protected?
What international installation, commissioning, and operator training services do you provide?
Can buyers conduct pre-shipment Factory Acceptance Testing (FAT) in Wuxi?
Explore Custom Industrial Line Configurations
Factory-direct metallurgy machinery built to your exact coil dimensions, yield strengths, and target daily output metrics.

China Manufacturer Of Slitting Line Manufacturers, Supplier
Turnkey high-speed slitting lines configured for heavy master coils, featuring interchangeable slitter heads and hydraulic recoiler tensioning.
Explore Line
High-Quality Professional Flying Shear Production Line
Synchronized continuous dynamic shearing eliminating surface scuffing on delicate automotive and prepainted coil applications.
View Flying Shear
CE Certification Manufacturer Of Cut to Length Line
Certified to EN safety and ISO quality standards, providing full-lifecycle structural durability and high precision blank stacking.
Get Certification Specs
High Strength Leveling Machine
Industrial multi-roll flattening cassettes engineered for heavy structural plate up to 25 mm thickness with full hydraulic roll bending control.
Select Capacity
Professional Straightening Machine
Eliminate residual coil stresses and curvature on high tensile steel strips before stamping, roll-forming, or laser processing.
Technical Details
Hot Rolled Plate Moving Shear Line
Accelerated hydraulic cutting bridge designed specifically for heavy-duty structural steel service centers operating 24/7 continuous output.
Explore Heavy Shear
Stainless Steel Uncoiling-Leveling-Shearing-Stacking Line
Automated vacuum-cup stacking arms, high-precision hydraulic guillotine, and rubber-lined pinch rolls for pristine mirror-finished sheets.
View Line Architecture
Hot Rolled Sheet Uncoiling Slitting & Recoiling Line
Integrated with high-capacity hydraulic scrap winders, quick-change arbor turrets, and automated turnstiles for seamless slit coil offloading.
Request LayoutReady to Engineer Your Next High-Performance Coil Line?
Consult directly with our metallurgical machinery specialists. Submit your coil specifications (thickness, width, yield strength, and target line velocity) to receive a custom 3D line layout and budgetary engineering proposal within 24 business hours.