
Engineered Coil Processing & Edge Correction Lines
Explore our certified edge straighteners, high-strength levelers, slitting systems, and high-speed moving shear configurations optimized for extreme yield strengths and continuous mill duties.
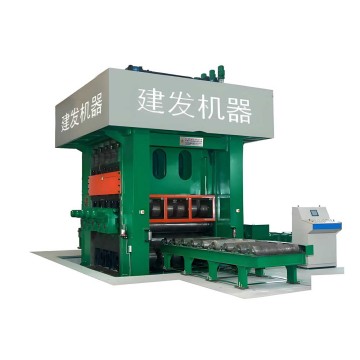
Heavy-duty multi-roll leveler with multi-zone back-up cassettes engineered to eradicate coil set, cross bow, and residual inner stresses.
Explore Specification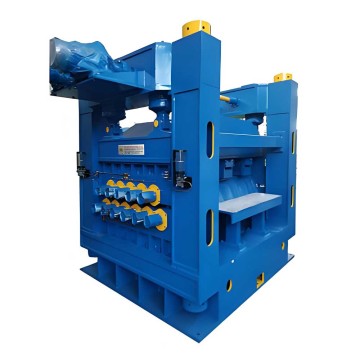
Precision calibrated edge and surface straightener providing sub-millimeter flatness tolerances for stamping, profiling, and laser fabrication.
Explore Specification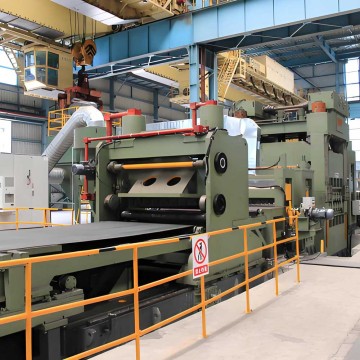
High-speed synchronized rotary shear line cutting heavy-gauge plate without stopping, engineered for maximum plant throughput and edge squareness.
Explore Specification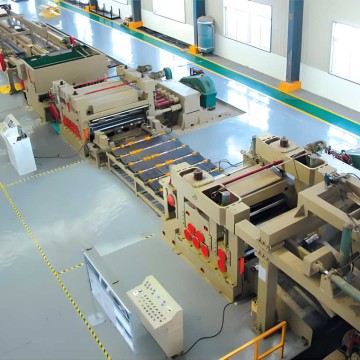
Zero-mar continuous surface protection line equipped with 6Hi precision leveling rolls and automated magnetic/vacuum sheet stacking cells.
Explore Specification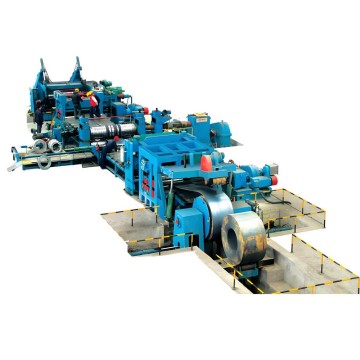
Hybrid production plant integrating precision rotary edge trimming, intermediate multi-roll leveling, and programmable high-accuracy blank shearing.
Explore Specification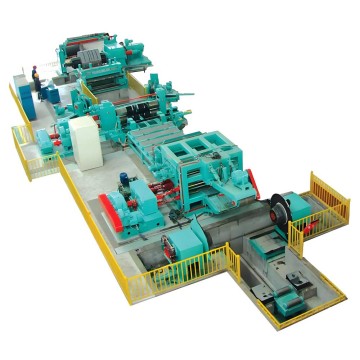
Equipped with ultra-rigid knife arbors and double eccentric clearance adjustment for zero-burr multi-strip separation at high line velocities.
Explore Specification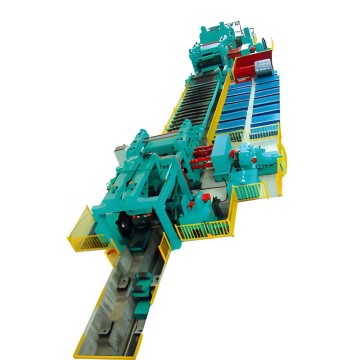
Configured specifically for ERW pipe and roll-forming feedstocks, featuring heavy-gauge hydraulic recoiler push-offs and active strip edge guide control.
Explore Specification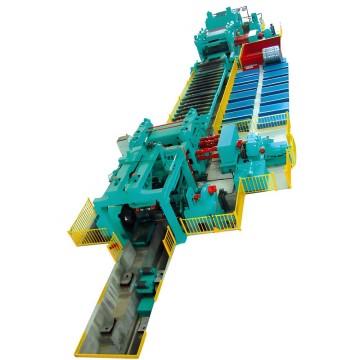
Extreme duty hydraulic leveling cassettes combined with automated precision stop-to-cut shears designed for high-strength steel coil handling up to 25mm.
Explore SpecificationRedefining Edge Straightener Engineering Under CE Directives
In modern high-speed roll forming, continuous ERW tube welding, and automotive AHSS blanking, edge curvature (camber) and residual lateral stresses are the primary causes of mill downtime, die jamming, and weld seams rejection. Wuxi Jianfa delivers CE-certified edge straighteners engineered to eliminate camber defects through closed-loop servo-hydraulic roll positioning.
The Mechanics of Lateral Camber & Roll-Bending Stress Relief
When metal coils are slit from master mother coils, non-uniform internal stress distributions cause lateral bow—commonly known as camber or sweep. Conventional pinch rolls cannot resolve this dimensional distortion. Our CE Certification Edge Straighteners utilize an array of horizontally oriented, precision ground carbide/hard-chrome rolls that exert progressive, alternating plastic bending beyond the strip's yield point (ReH).
By combining multi-point hydraulic servo backup blocks with high-precision load cells, the machine recalculates the elastic-plastic deformation curve in real time. The strip exits the straightening cassette with edge straightness deviations reduced to under 0.2mm per meter, providing ideal feeding tolerances for downstream laser blanking and automated roll formers.
CE Certification Framework & EU Machinery Directives
Procuring industrial machinery from China requires verifiable adherence to strict international safety directives. Wuxi Jianfa designs, manufactures, and documents each edge straightener in total compliance with harmonized European standards.
2006/42/EC Machinery Directive
Full risk assessment according to EN ISO 12100:2010. Mechanical assemblies integrate dual-circuit hydraulic holding valves, mechanical interlocks on straightening roll cassettes, and physical intrusion light curtains.
- Harmonized Standard EN ISO 12100
- Safety Relay Class Safety Category 4 (PLe)
- Documentation Full Technical File (TCF)
EN 60204-1 Electrical Safety
Standardized electrical enclosure layout with Siemens / Schneider / Omron PLC architectures. Features IP54/IP65 protection, segregated high-voltage drive conduits, and verified earth-bonding continuous loops.
- Enclosure Rating Rittal IP55 Standard
- EMC Directive 2014/30/EU Validated
- Low Voltage Directive 2014/35/EU Tested
Localization & Remote Telemetry
Full English / German / Spanish HMI interface configurations. Integrated VPN gateways provide secure, encrypted remote access for diagnostics, roll gap calibration, and firmware lifecycle management.
- Remote Bridge Secomea / Siemens eWON
- HMI Customization Multi-lingual Touchscreen
- On-Site Engineer Schengen/US Visa Ready
The Future of Metal Edge Straightening Technology
The evolution of edge straighteners is shifting from empirical operator manual adjustments toward closed-loop autonomous leveling driven by AI-powered vision inspection and dynamic hydraulic response.
Optical Laser Camber Scanning
Integrating high-frequency 2D laser triangulation scanners at both entry and exit throats. The optical array captures continuous edge profiles at up to 120m/min, automatically feeding deviation delta values to the PLC.
Dynamic Servo Wedge Actuation
Replacing traditional AC gearmotor screw jacks with high-speed servo-hydraulic proportional valves. Adjustments to individual straightening roll depths occur dynamically without decelerating the coil line.
Predictive Roll Wear Diagnostics
Embedded piezoelectric accelerometers and continuous thermal monitoring on all journal bearings. Edge roll degradation and localized galling are predicted before micro-cracks imprint on strip edges.
| Straightening Parameter | Light-Gauge Precision Series | Medium Gauge Coil Processing | Heavy-Plate Mill Duty Series |
|---|---|---|---|
| Strip Thickness Range | 0.3 mm – 3.0 mm | 2.0 mm – 8.0 mm | 6.0 mm – 25.0 mm |
| Strip Width Compatibility | 50 mm – 600 mm | 150 mm – 1650 mm | 300 mm – 2200 mm |
| Maximum Material Yield Strength | Up to 600 MPa | Up to 980 MPa (AHSS) | Up to 1250 MPa (Q&T Steels) |
| Straightening Roll Count | 7 to 11 Horizontal Rolls | 9 to 13 Opposed Rolls | 7 to 9 Heavy Forged Rolls |
| Roll Hardness / Metallurgy | GCr15 / 60-62 HRC (Hard Chrome) | 42CrMo Forged / Induction 62 HRC | Cr12MoV / Dual Heat-Treated |
| Linear Process Velocity | Up to 120 m/min | Up to 80 m/min | Up to 40 m/min |
| CE Safety Certification | Fully Certified (EN ISO 13849-1) | Fully Certified (EN ISO 13849-1) | Fully Certified (EN ISO 13849-1) |
Engineered Sector Solutions for Demanding Tolerances
Across diverse downstream fabrication sectors, precise edge condition determines whether continuous production succeeds or suffers costly die failures and weld porosity.
Automotive AHSS Body-in-White
Dual-phase (DP) and Martensitic automotive sheets experience aggressive camber after multi-strand slitting. Jianfa edge straighteners eliminate edge curvature prior to progressive die stamping, preventing transfer robot misfeeds.
Solar Tracking & C-Channel Purlins
Solar torque tubes and long roll-formed profiles require strict straightness across 12-meter lengths. Our in-line edge conditioning prevents profile corkscrewing and twist during cold roll forming.
Shipbuilding & Offshore Heavy Plate
Processing high-tensile structural steel plates up to 25mm thickness. Straightened edge geometries ensure precise fit-up during automated submerged arc welding (SAW) on ship hulls and monopiles.
ERW Tube & Pipe Mill Lines
Eliminating edge camber is critical to preventing offset edges at the high-frequency induction welding station. Jianfa equipment guarantees symmetrical welding V-groove presentation.
China Factory 4.0: Supply Chain Resilience & Precision Machining
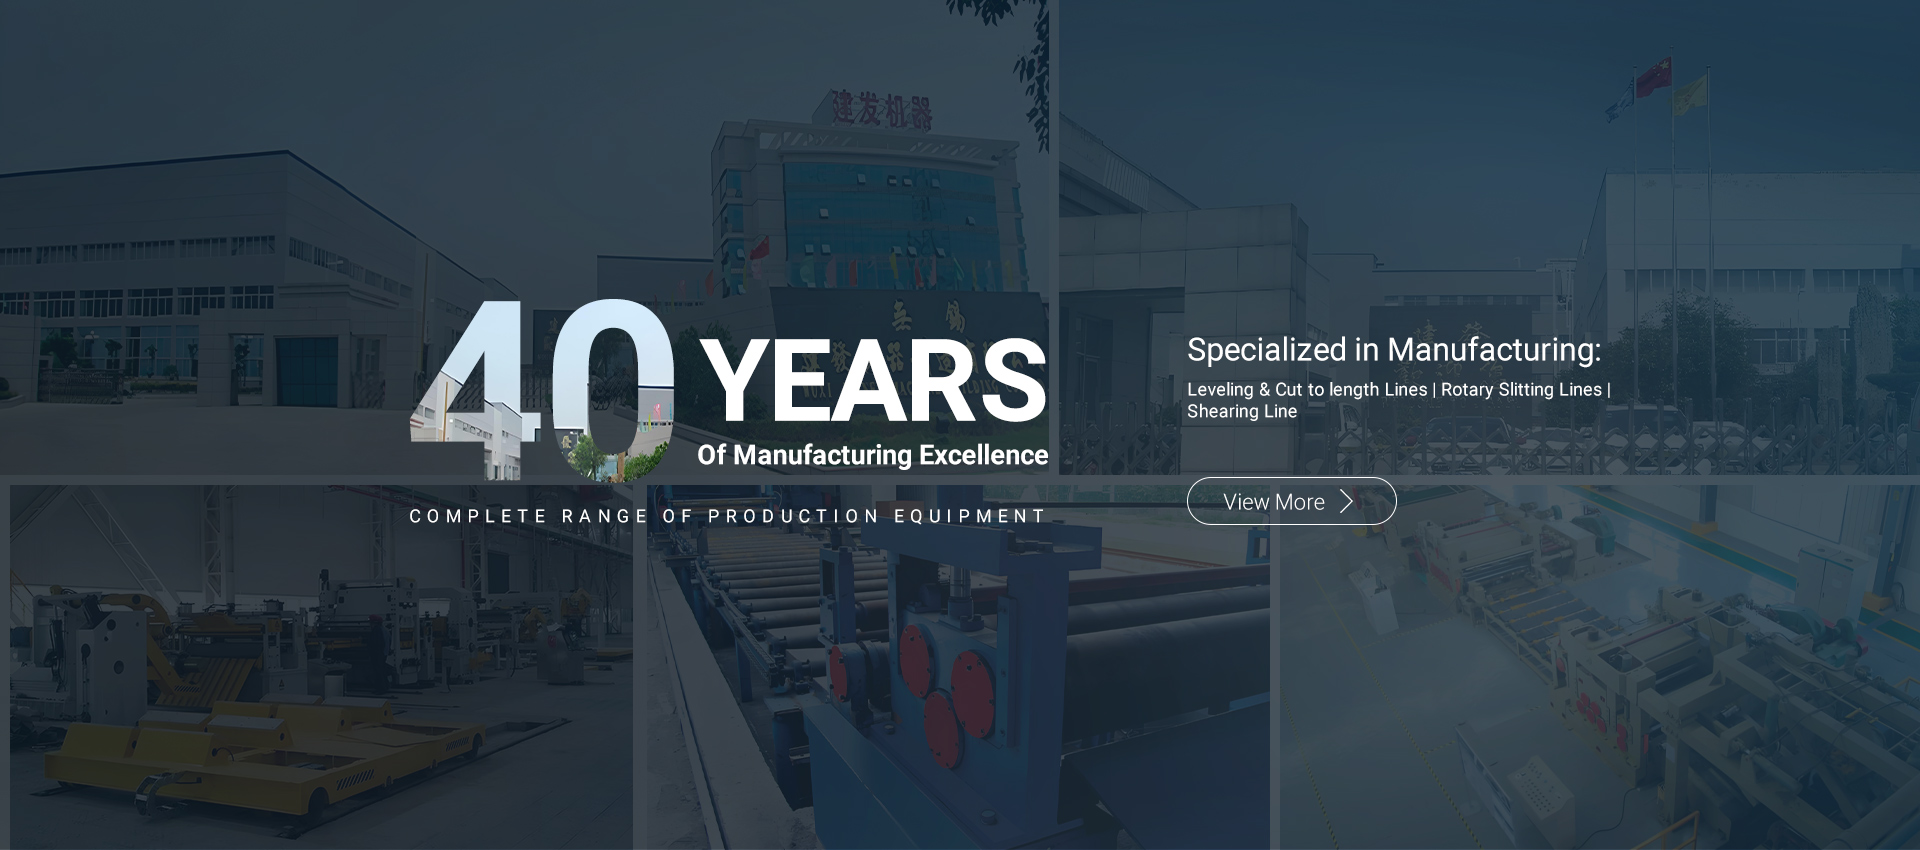
Located in the heart of the Yangtze River Delta industrial corridor in Wuxi, Jiangsu, Wuxi Jianfa combines four decades of metallurgical machine building with vertically integrated CNC manufacturing.
Full In-House Machining from Raw Forgings to Commissioned Cells
Unlike assembly-only machine builders who outsource critical components, Wuxi Jianfa executes rough machining, stress-relief annealing, induction hardening, finish CNC gantry milling, and cylindrical grinding under our own 40,000 square meter factory roof.
Our facility houses large-scale 5-axis CNC horizontal boring centers and heavy coordinate measuring machines (CMM). Every straightener roll journal, cassette housing, and guide frame is verified for geometric parallelism to within ±0.015mm over 3000mm spans.
Global Enterprise Procurement: Essential RFQ Parameters
To receive an accurate engineering calculation and technical proposal from our engineering office, global procurement teams are encouraged to define the following parameters in their inquiry:
1. Material Metallurgical Specs
Specify grade classification (e.g., DIN EN 10149-2, ASTM A1011), minimum/maximum yield strength (Rp0.2), ultimate tensile strength (Rm), and surface condition (dry, oiled, pickling, galvanizing).
2. Dimensional Boundaries
Indicate min/max strip thickness, incoming width range, incoming maximum edge camber per meter (e.g., 5mm in 2000mm), and target post-straightened residual tolerance limit.
3. Production Integration
Specify line speed requirements, line direction (left-to-right or right-to-left), electrical grid rating (e.g., 400V 50Hz / 480V 60Hz), and preferred automation brands (Siemens, Rockwell, Rexroth).
Frequently Asked Engineering Questions
Detailed insights from our chief mechanical design engineers addressing coil camber, machine sizing, and certification mandates.
A standard leveler features horizontally stacked rolls designed to eliminate cross-bow and coil set by bending the sheet across its thickness axis. An edge straightener utilizes vertically stacked or opposed horizontal rolls that apply lateral forces across the width axis, plasticizing the strip edges to eliminate edge camber (sweep) and lateral bow that traditional levelers cannot correct.
All equipment destined for the EU, UK, or overseas markets complies with Directive 2006/42/EC. We supply comprehensive Technical Construction Files (TCF), Declaration of Conformity (DoC), verified ISO 13849-1 electrical safety schematics, emergency stop redundancy with monitored valves, and certified bilingual operation manuals.
Yes. We engineer self-contained edge straightener cassettes complete with independent servo pull-through drives or idle tracking rolls. These integrate seamlessly between loop pits and roll forming entry tables, synchronizing via fieldbus protocols (Profinet, EtherCAT, or Ethernet/IP).
For bright-finish stainless steel, pre-painted metal, and aluminum coils, straightener rolls are precision super-finished (Ra < 0.1μm) and hard-chrome plated or sleeved with high-grade polyurethane / non-marking alloys. Intermediate cleaning brushes remove abrasive scale particles during continuous processing.
Factory Direct Coil Processing Equipment Specifications
Review comprehensive technical proposals, capacity matrices, and video trials of our proven coil line models.

Engineered for uncoiling, high-precision leveling, measuring, and auto-stacking heavy metal coils into tight-tolerance sheet packages.
Request Full Quotation
Continuous dynamic shearing system that synchronizes cutting motions with line speeds up to 100m/min without stopping the strip.
Request Full Quotation
Rigid rotary slitter head paired with dynamic tensioning pads, automated scrap ballers, and precision recoil tension mandrels.
Request Full Quotation
Equipped with 4Hi/6Hi configurations and individual motorized back-up roll adjustments to eliminate complex 3D shape defects.
Request Full Quotation
Multi-roll mechanical straightener providing consistent stress relief and edge profile conditioning for automotive tier suppliers.
Request Full Quotation
Continuous heavy-plate cutting line engineered for maximum uptime, rigid edge squareness, and automated palletized bundling.
Request Full Quotation
High-precision surface protection configuration preventing scratching on No.4, BA, and hairline finishes during high-volume processing.
Request Full Quotation
Heavy duty uncoiling and rotary slitting line capable of processing high-tensile structural carbon steel master coils up to 35 tons.
Request Full QuotationConsult Directly with Jianfa Senior Machine Building Engineers
Avoid communication friction through middlemen. Send your coil material data sheet, required strip edge tolerances, and line speed requirements directly to our technical application team in Wuxi. We generate verified 2D line layouts, power consumption estimates, and CE conformity plans within one business day.
Wuxi Jianfa Machine-Building Co., Ltd.
Headquarters & Works: No. 58 Qunxing Road, Meicun, Xinwu District, Wuxi, Jiangsu, China
Direct Engineering Line: +86-510-88151451 / +86-139-2116-6015
Direct Sales Email: [email protected] | [email protected]
Port Accessibility: 130 km to Shanghai Port · Rapid Containerized & Breakbulk Vessel Dispatch