
Featured Coil Slitting & Cut-to-Length Production Equipment
Every system is custom-configured around your metallurgy, shear-yield parameters, strip burr tolerances, and production throughput targets with factory-direct CE compliance.

High Strength Leveling Machine
Engineered with multi-roll cassette technology to eliminate internal residual stresses, coil set, and edge waves in ultra-high yield strength plates.

Professional Straightening Machine
Precision calibration for structural cold-rolled and hot-rolled coils, securing flat, stress-relieved blanks prior to progressive stamping or roll forming.

Hot Rolled Plate Moving Shear Line
Continuous dynamic shearing traveling synchronously with the moving metal strip to achieve extraordinary throughput with zero start-stop friction marks.

Stainless Steel Uncoiling-Leveling-Shearing Line
Surface-critical processing designed with non-marking polyurethane rollers and automatic pneumatic stacking for 2B, BA, and polished sheets.

Combined Slitting & Cut-To-Length Line
Compact hybrid architecture performing multi-strand lengthwise slitting and cross-cutting within a single automated line footprint to optimize floor space.

Hot Rolled Uncoiling, Slitting & Recoiling Line
Rotary slitter head housing precision-machined forged alloy shafts, dynamic knife clearance adjusters, and low-noise continuous edge scrap winders.

Heavy Gauge HR Slitting-Recoiling Line
Built for structural tube manufacturing and mill-grade plate processing, handling strip thicknesses up to 25mm with superior recoil edge alignment.

HR Uncoiling-Leveling-Shearing-Stacking Line
Integrated closed-loop system equipped with laser length measurement, hydraulic swing-beam shear, and magnetic drop-stacking for zero-defect sheets.
The Global Coil Slitting Sector: Macro Shifts & Technical Demands
In modern metallurgical manufacturing, coil slitters are no longer mere standalone rotary knives. They represent mission-critical precision capital equipment at the intersection of material science, automation, and safety compliance.
Advanced High-Strength Steels (AHSS)
Global automotive lightweighting mandates have forced service centers to transition from standard mild steels to dual-phase (DP), complex-phase (CP), and martensitic steels reaching tensile strengths exceeding 1200 to 1500 MPa. Slitting these alloys without edge cracking, excessive camber, or rapid arbor deflection requires severe machine frame rigidity and dynamic hydraulic knife clearance compensation.
E-Mobility & Grain-Oriented Silicon Steel
The global expansion of EV traction motor manufacturing and high-voltage grid transformer substations demands ultra-precision slitting of ultra-thin electrical steels (0.15mm to 0.35mm). Any minute knife burr exceeding 10 microns causes magnetic flux distortion and eddy current energy losses. Modern slitters must operate with arbor axial and radial runout below 0.003mm.
Scrap Reduction & Yield Optimization
With volatile raw steel coil prices, downstream steel service centers operate on microscopic operating margins. Edge-trim scrap must be reduced from traditional 20mm margins down to 5mm to 8mm per side. This demands sophisticated optical edge-tracking, continuous loop sensors, and self-regulating tensioners that prevent slippage and eliminate surface friction scuffing.
CE Certification: Engineering Beyond the Compliance Label
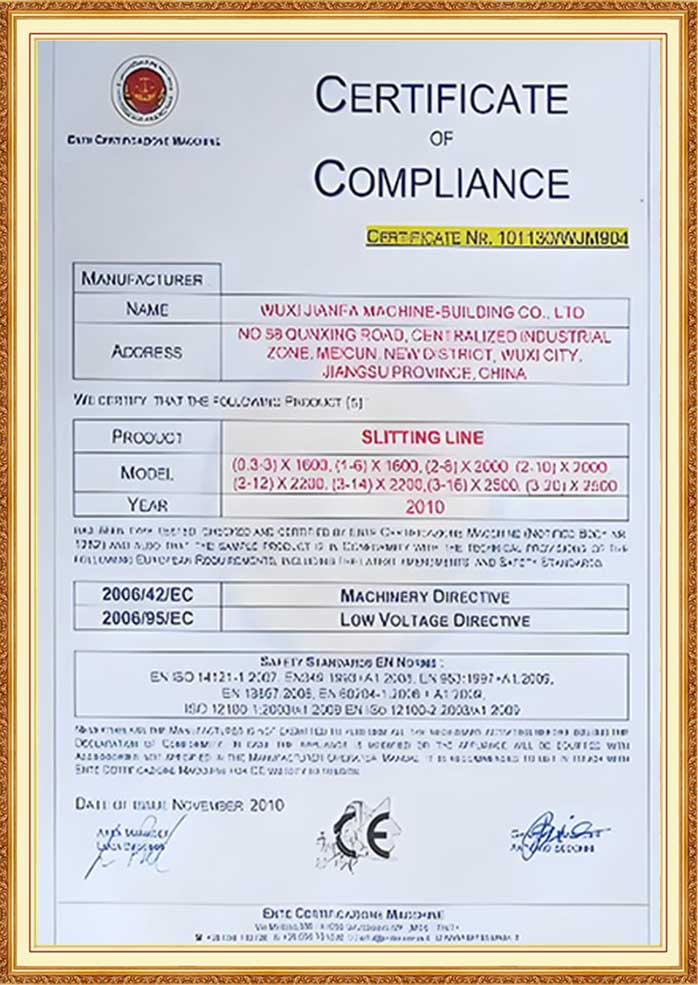
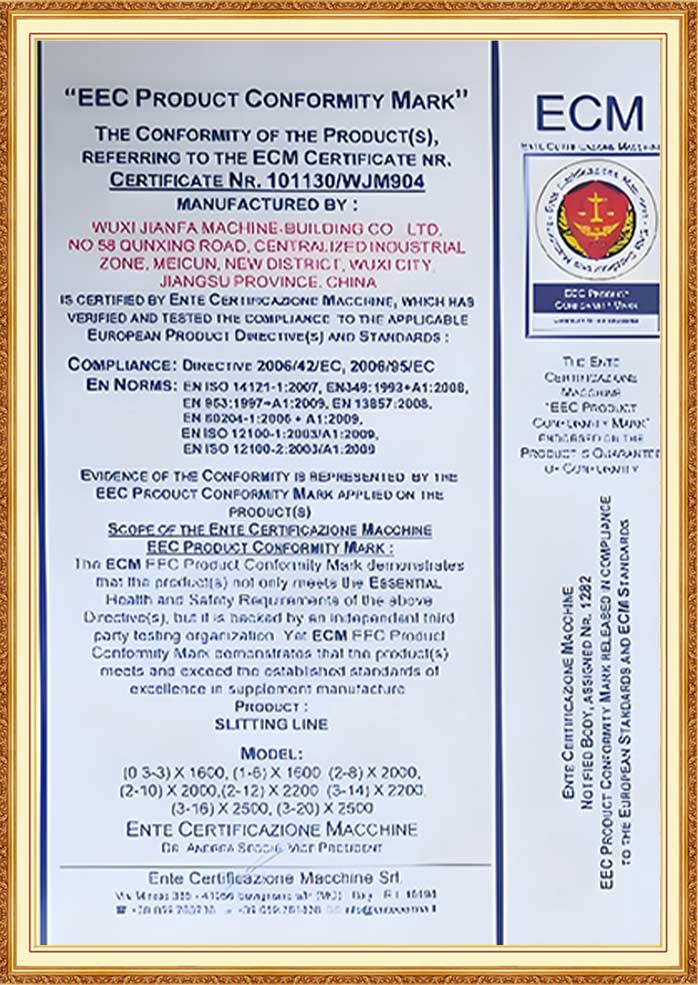
For multinational processors, the CE mark on a slitting line is not just a commercial formality; it is a legally binding guarantee of structural integrity, operational functional safety, and risk abatement under rigorous European standards.
Machinery Directive 2006/42/EC & Harmonized Standards
Wuxi Jianfa custom builds and inspects every slitter according to the stringent provisions of EN ISO 12100:2010 (Safety of machinery — General principles for design, risk assessment and risk reduction). Key mechanical interventions include:
- Hydraulic Mechanical Locking Pins: Dual physical anti-drop locks on pay-off uncoiler mandrels and coil car scissor jacks to prevent catastrophic hydraulic seal failure hazards.
- Interlocked Safety Enclosures: Category IV light curtains and dual-channel safety-switch perimeter fencing enclosing the high-speed slitter arbor, looper pit, and recoiler nip point.
- Low Noise Hydraulic Power Units (HPU): Engineered under 78 dB(A) acoustic thresholds, conforming to European workplace occupational health noise level regulations.
Functional Safety (EN ISO 13849-1) & Electrical Directives
Uncontrolled recoil strip slippage or uncoiler brake release in a high-speed slitting line (operating at 120-250 m/min) creates immense physical hazard. Our CE-marked lines implement:
- Performance Level (PL d / PL e) Architecture: Redundant Siemens or Schneider safety PLCs executing emergency stops, arbor jog modes, and safe-limited-speed (SLS) during manual knife threading.
- Low Voltage Directive (2014/35/EU): Fully partitioned electrical cabinets with IP54 isolation, thermal dissipation analysis, and touch-safe terminal block assemblies.
- EMC Directive (2014/30/EU): Industrial line reactors, shielded servo cables, and ferrite chokes eliminating high-frequency harmonic distortion from multi-axis AC variable frequency drives.
Verified Manufacturing Certifications & Institutional Credentials
Engineering Matrix: Slitting Line vs. CTL vs. Flying Shear
Selecting the optimum coil conversion line requires balancing coil mechanical yields, edge strip specifications, burr limits, and downstream manufacturing cycles. Compare the design parameters below:
| Performance Dimension | High-Precision Slitting Line | Start-Stop Cut-to-Length (CTL) | Synchronous Flying Shear Line |
|---|---|---|---|
| Primary Finished Geometry | Multi-strand narrow strips rewound on recoiler cores | Flat rectangular panels/plates stacked on pallets | High-speed dimensioned flat sheets stacked continuously |
| Strip Kinematics at Cut | Continuous rotary shear velocity (0–220 m/min) | Discontinuous start-stop with hydraulic feeder dwell | Continuous non-stop strip flow (shear matches linear web speed) |
| Burr Height Ratio Limit | < 5% to 7% of nominal strip gauge (knife clearance) | < 8% to 10% on plate cross-shear cut face | < 6% with dynamic rotary or crank acceleration shear |
| Thickness Capability | 0.15mm – 16.0mm (alloy and frame dependent) | 0.5mm – 25.0mm (heavy structural plate) | 0.3mm – 6.0mm (sheet metal and light gauge plate) |
| Downstream Ecosystem | ERW tube mills, roll formers, automotive stamping | Heavy fabrication, laser cutting centers, panel builders | High-volume white goods, appliance shells, automotive blanks |
| Critical Design Subsystems | Shimless tooling arbors, tension drag pad/belt, looper pit | 4-high / 6-high leveler cassettes, servo roll feeder | Direct-drive dynamic servo rack, rotary drum cutter assembly |
Rotary Arbor Deflection Control
Our slitter arbors are machined from forged 42CrMo/40CrNiMo alloy steel, through-hardened and ground to surface roughness Ra 0.2µm. Preloaded precision four-row cylindrical roller bearings limit total radial and axial arbor runout to within 0.003mm, eliminating knife overlap breathing during high-speed runs.
Dual-Loop Tensioning Technology
Different strip strands across a wide slitted master coil inherently exhibit slight thickness variations due to mill crown. We incorporate dual tension stands (pneumatic felt pad drag stands combined with dynamic tension roll bridles) to ensure each strand maintains uniform recoiling tightness without slippage marks.
Rapid Slitter Head Changeover
To eliminate costly downtime in job-shop steel centers, Jianfa equips systems with a dual-head or turnstile slitter design. While one arbor assembly is slitting production coils, the operator pre-sets knives and polyurethane strippers on the standby head, enabling complete head exchange in under 8 minutes.
Specialized Slitting Solutions: Application-Specific Engineering
Material characteristics govern slitting mechanics. Wuxi Jianfa builds bespoke slitting architectures targeted at demanding downstream application sectors worldwide.
Automotive Body-in-White (BIW)
Processing exposed outer panels requires zero tolerance for slivers, burrs, or roll scratching. Jianfa slitting lines feature non-contact eddy-current edge inspectors, chromium-plated guide rolls, and dust-evacuation suction hoods along the cut point to maintain pristine 6000-series aluminum and galvannealed surfaces.
Electrical Silicon Transformer Core
Slitting CRGO (Cold-Rolled Grain-Oriented) and CRNGO silicon steels requires specialized tungsten carbide rotary slitting knives. Our precision arbors maintain minimal knife engagement overlap, reducing deformation stress and preventing magnetic core degradation in distribution transformers.
Tube Mill & Structural Profile Supply
High-volume welded tube fabrication demands slit mults with pristine edge squareness and minimal edge strain-hardening to assure full-penetration HF welding. Our lines incorporate heavy edge-break deburring units and synchronized multi-arm recoiling turnstiles.
Architectural Stainless Steel
Mirror (No. 8), hairline, and embossed stainless sheets (304, 316, 430) require synchronized automatic PVC/PE protective film applicators. Jianfa integrates top-and-bottom laminators with tension-regulated bubble-free uncoiling ahead of rotary knife entry.
Engineering Roadmap: Next-Gen Smart Slitting Architecture
As smart manufacturing transforms metal forming, Wuxi Jianfa is pushing the frontier of closed-loop cyber-physical slitting machinery to eliminate human setup error and extend tooling lifecycles.
AI Robotic Knife Positioning
Replacing manual arbor stacking with high-precision gantry robot arms that read incoming work orders directly from plant MES/ERP systems. Tooling rings, shimless polyurethane spacers, and knives are placed with 0.005mm accuracy, cutting arbor re-tooling intervals from 45 minutes down to under 4 minutes.
Acoustic Emission Wear Telemetry
Integrating high-bandwidth piezoelectric acoustic sensors directly onto slitter bearing pedestals. By analyzing high-frequency micro-acoustic waves during material fracture, our edge telemetry algorithms detect blade chipping, excessive dulling, or micro-clearance shifts hours before edge burrs become visible.
Cloud-Linked Predictive Diagnostics
Full IoT integration over secure industrial MQTT protocols allows Jianfa engineering specialists in Wuxi to monitor vibration spectra, motor thermal signatures, and hydraulic proportional valve health on overseas installations, delivering remote diagnostics and zero-unplanned-downtime maintenance programs.
Technical & Commercial FAQ: Deep Metallurgical Insights
Direct, engineering-level answers to the operational, technical, and regulatory questions most frequently submitted by plant managers and procurement directors.
What coil processing equipment does Wuxi Jianfa manufacture?
We design, cast, machine, assemble, and commission complete coil processing systems: precision rotary slitting lines (for metal strips), cut to length (CTL) lines, high-speed flying shear lines, heavy-duty 4-high and 6-high leveling machines, multi-roll plate straightening machines, and continuous hot-dip galvanizing lines. Equipment can be commissioned as complete turnkey plants or supplied as modular machine units to modernize existing customer processing lines.
Which metal alloys and mechanical strength grades can your slitters process?
Our lines are engineered to process hot-rolled structural steel, cold-rolled mild steel, galvanized/galvalume coils, austenitic and ferritic stainless steel (200, 300, 400 series), electrical silicon steel, and non-ferrous alloys such as 1000 to 6000-series aluminum, brass, and copper. We regularly build heavy-gauge slitting systems rated for yield strengths up to 980 MPa and specialized high-strength steel (AHSS/UHSS) configurations up to 1500 MPa tensile strength.
How do you calculate proper knife horizontal clearance and blade overlap?
Horizontal knife clearance is governed strictly by material gauge and tensile yield. For cold-rolled mild steel, horizontal clearance is typically calibrated between 7% to 10% of nominal thickness; for high-tensile steels or stainless, it ranges from 11% to 15%; while for soft aluminum alloys, clearances are set between 5% to 8%. Proper clearance induces 1/3 clean shear depth and 2/3 controlled tensile fracture, eliminating rolled-edge camber and excessive micro-burrs.
How does Wuxi Jianfa guarantee compliance with European CE regulations?
Compliance is engineered into the mechanical, electrical, and hydraulic drawings from initial design rather than retrofitted. We provide a complete Technical Construction File (TCF), valid EC Declaration of Conformity under Machinery Directive 2006/42/EC, full electromagnetic immunity testing reports (EMC 2014/30/EU), and third-party certified functional safety validation documents covering emergency circuit performance levels (EN ISO 13849-1).
What specific parameters are needed to issue a definitive engineering proposal?
To produce an exact layout, power calculation, and cost quotation, our engineers need: (1) Material grade, yield strength, and shear strength; (2) Thickness range (min/max) and coil width range; (3) Master coil weight (max) and inside/outside diameter; (4) Minimum target slit strip width and maximum number of simultaneous cuts; (5) Required line velocity (e.g., 60, 120, or 180 m/min); and (6) Local factory grid voltage, frequency, and space limitations.
How does after-sales installation, operator training, and spare parts supply work overseas?
We deploy senior mechanical commissioning engineers and electrical automation specialists directly to buyer sites globally. Our overseas commissioning protocols encompass foundation alignment verification, uncoiler-slitter-recoiler optical center-line leveling, cold/hot dry runs, live production tuning, and comprehensive multi-tier operator and maintenance personnel safety training. Key wear components (knives, strippers, spacers, hydraulic filters) are stocked for rapid international air dispatch.
Direct Factory Manufacturing Base: Wuxi Jianfa Machine-Building Co., Ltd.
Established in the early 1980s, Wuxi Jianfa is designated as a national key developing enterprise in China's metallurgical machinery sector. Operating from our own modern 40,000 square meter industrial manufacturing facility in Wuxi's Xinwu District (Jiangsu Province), we ensure end-to-end design, CNC heavy boring, gantry milling, heat treatment, and pre-shipment live material trials under one roof.
Factory Audits & Inspection
Overseas buyers and accredited third-party inspection agencies (SGS, TÜV, Bureau Veritas) are welcomed to inspect raw forgings, dimensional tolerances, and full line running tests prior to ocean export packing.
Request Factory Audit ProtocolExplore Our Heavy-Duty Industrial Line Catalog
Select any specialized processing configuration below to review customized line schematics, dynamic coil capacities, and standard CE equipment specifications.

CE Certified Cut to Length Line
Heavy-duty, high-precision leveling and shearing lines meeting full European CE safety standards, optimized for service centers and mills.

Professional Flying Shear Line
Continuous dynamic strip tracking for ultra-high-speed blanking without surface scuffing or hydraulic dwell delays.

China Slitting Line Manufacturer
Factory-direct high precision slitting lines from Wuxi, featuring robust construction, rapid tooling changeovers, and long working life.
Heavy Plate Moving Shear Line
Engineered for hot-rolled steel plates up to 25mm thickness, combining heavy-duty levelers with traveling shear car carriages.
Stainless Precision Cut to Length Line
Designed specifically for polished stainless steel coils with non-marking rubberized feed rolls and air-cushioned sheet stackers.
Sheet Slitting & Recoiling Systems
High-efficiency coil uncoiling, multi-strand slitting, and tight recoiling lines with motorized scrap ballers and auto-tensioning.
Multi-Roll High Strength Leveler
Deep mechanical plasticity deformation rollers that eliminate internal residual tension, ensuring completely flat laser-cuttable sheet blanks.
Turnkey HR Slitting Production Line
Heavy structural steel slitting lines configured for heavy strip producers, pipe manufacturers, and large-scale metal distribution hubs.