
Plate Leveling

Factory-direct engineered processing lines custom built for stainless steel, cold-rolled, hot-rolled, and advanced high-strength steel (AHSS) coils.







A comprehensive industrial whitepaper on mechanical rigidity, knife tooling clearance dynamics, and lifecycle total cost of ownership (TCO) for global steel processors.
For modern tier-1 automotive stampers and electrical transformer laminators, sheet metal coil slitting tolerance is strictly regulated. High-precision slitter arbors with dual-tapered roller bearings limit radial runout to less than ±0.003 mm, keeping edge burr under 3% of total strip thickness even at 200 m/min continuous line speeds.
Unscheduled downtime during slitter tooling changeovers severely impedes operating profitability. Turnkey CE-certified systems deploy dual-head or quadruple-turret rotary slitter designs. Tooling configurations are programmed off-line; shifting between cut profiles occurs in under 180 seconds via motorized hydraulic traversal indexing.
Importing capital metallurgical machinery into the European Economic Area demands full conformity with EN ISO 13849-1 (Safety-Related Parts of Control Systems, PL-e rating). Jianfa integrates Category 4 light curtains, hydraulic safety valve locking circuits, sound enclosures (<78 dB), and interlocked perimeter guarding natively into electrical blueprints.
Tailoring drive kinematics, tension leveling modules, and recoiler tensioning brakes to the distinct physical yield parameters of diversified metal grades.
Processing Dual-Phase (DP) and Martensitic steels up to 1200 MPa yield strength generates extreme separating forces on slitter arbors. Jianfa implements anti-deflection hydraulic locking housings and Tungsten Carbide tooling sleeves, eliminating slitter shaft bend and edge micro-cracking across high-stress blanks.
Grain-oriented (CRGO) and non-oriented (CRNGO) electrical steels demand zero residual stress and edge burrs under 0.01 mm to preserve magnetic flux and prevent eddy current losses. Our ultra-precision slitting lines feature specialized servo loop pits, optical edge guiding, and non-contact web tension brakes.
Architectural appliances, mirror-polished SUS304/316, and aerospace-grade aluminum sheets mandate defect-free surface preservation. We utilize polyurethane-coated pinch rolls, paper interleave applicators, protective film applicators, and pad-tensioning units with pneumatic belt-bridles to eliminate scratch marks.
| Equipment Model / Line Classification | Strip Thickness Range | Max Coil Width | Line Speed Performance | Primary Industrial Applications |
|---|---|---|---|---|
| Light Gauge High-Speed Slitter | 0.15 – 2.0 mm | 600 – 1,600 mm | Up to 300 m/min | Silicon steel cores, home appliances, auto body skins |
| Medium Gauge Precision Slitter | 0.8 – 6.0 mm | 1,000 – 2,000 mm | Up to 180 m/min | Tube & pipe production, roll forming, metal chassis |
| Heavy Gauge Rotary Slitting Line | 3.0 – 16.0 mm | 1,200 – 2,200 mm | Up to 80 m/min | Structural hollow sections, shipyards, pressure vessels |
| Combined Slitting & Cut-To-Length Line | 0.5 – 4.0 mm | 800 – 1,800 mm | Up to 120 m/min | Multi-format distribution steel service centers |
Transitioning from reactive mechanical shearing to deterministic, sensor-driven digital metallurgical execution.
Real-time optical cameras scan slit edges at high frame rates, automatically detecting knife wear patterns, burr height deviations, and edge camber before out-of-spec strips reach the recoiler mandrel.
Individual strip tension variance on multi-slit coils causes loose windings on thin gauges. Our proprietary hydraulic tension separators and multi-stage drag boxes calculate reel radius expansion in microsecond steps.
Fully compliant with OPC-UA protocols. Our Siemens or Rockwell Automation control suites interface directly with corporate SAP/Oracle ERPs, streaming coil weight, scrap tare weight, yield yield rates, and MTBF diagnostics.
Common DC-bus drive topologies capture mechanical braking energy generated by the uncoiler back-tension drag motor and feed it straight into the main recoiler drives, cutting total kilowatt-hour draw by up to 28%.
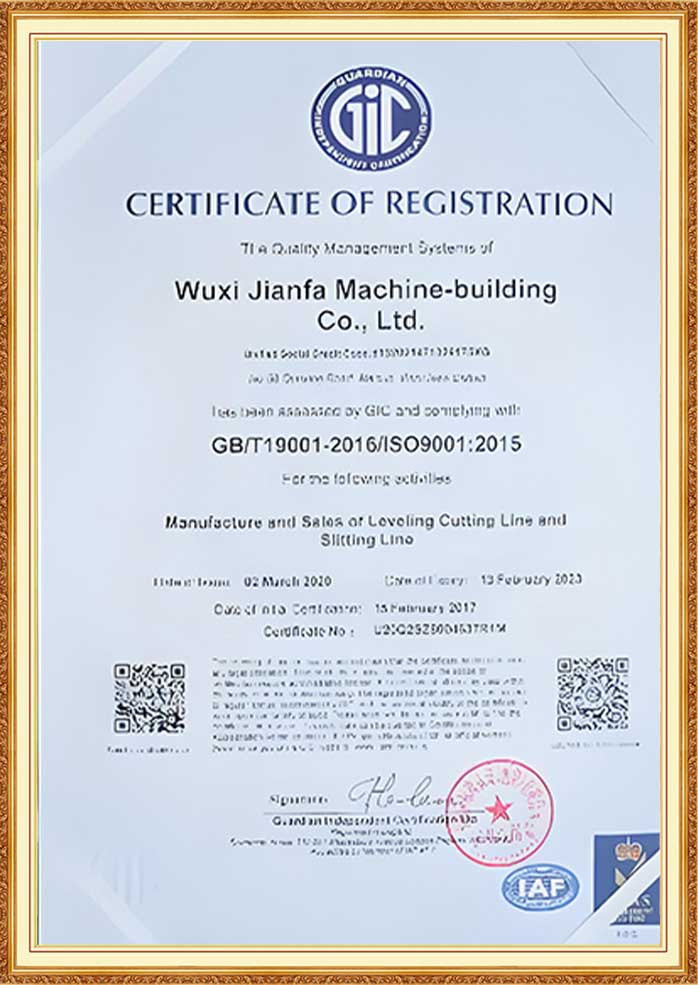
From European CE mark harmonization to UL electrical panels, ISO 9001 quality audits, and on-site commissioning across 30+ industrial countries.
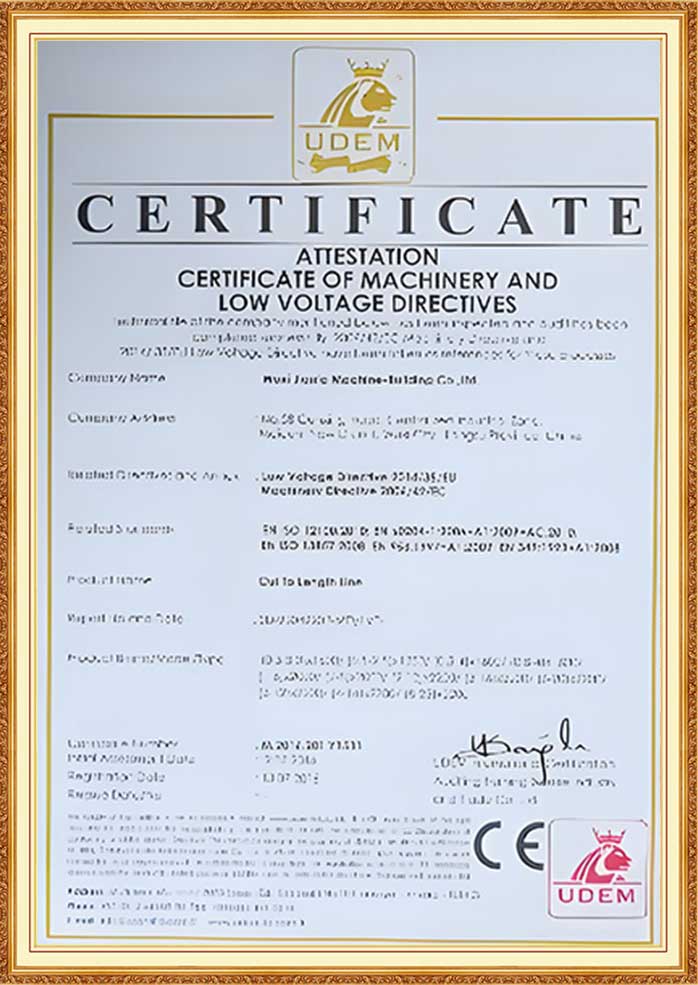
Every CE-badged metal slitting line manufactured at our 40,000 m² Wuxi campus complies fully with the EU Machinery Directive (2006/42/EC), Low Voltage Directive (2014/35/EU), and Electromagnetic Compatibility Directive (2014/30/EU). Critical hydraulic lines integrate dual-channel non-return check valves and emergency mechanical pin-locks on cutter heads.
Overseas heavy metallurgical investments require uninterrupted technical responsiveness. Jianfa maintains factory-trained commissioning specialists who execute foundation surveys, alignment anchoring, trial slit calibration, and native operator training globally across North America, Europe, Central Asia, the Middle East, and Southeast Asia.
Four decades of verifiable engineering consistency verified by national and international standardization bodies.
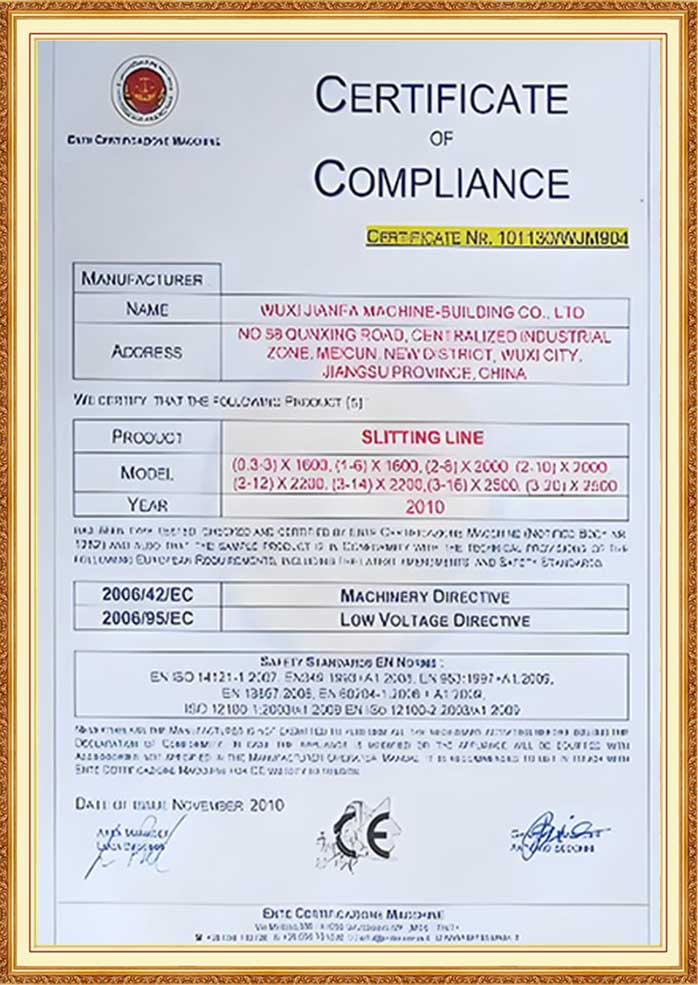
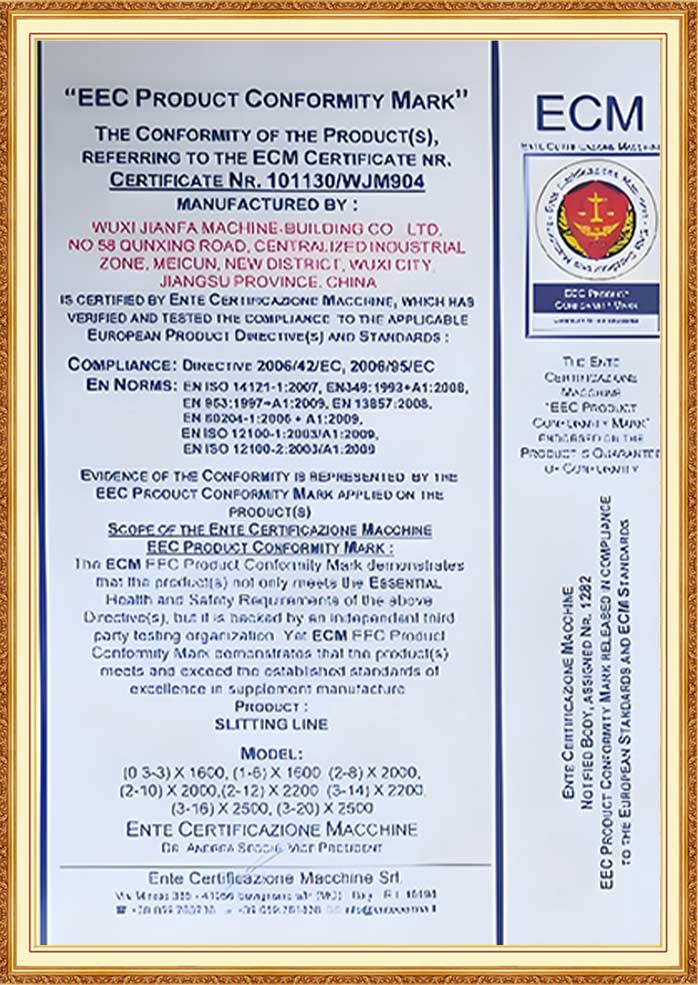
Precise operational insights provided by our metallurgical design bureau for project directors, plant managers, and equipment buyers.
Explore our field-proven production lines engineered to deliver superior strip edge geometry, tight coil rewinds, and non-stop operational endurance.
Eliminate trading markups. Submit your steel or aluminum coil dimensions, material yield strength, and annual tonnage targets. A senior metallurgical equipment designer will prepare a formal CAD layout and technical proposal within 24 hours.