
Featured Metal Coil Slitting & Processing Machinery
Direct from our specialized 40,000 m² heavy machinery plant: engineered for maximum edge cleanliness, superior tension control, and scratch-free processing across aluminum alloys, carbon steel, and stainless strip.
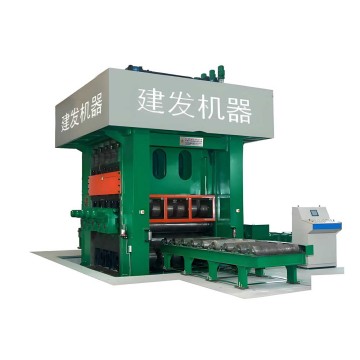
High Strength Leveling Machine
Engineered for deep stress-relieving and eliminating coil curvature in high-tensile alloys and heavy gauges.
View Specifications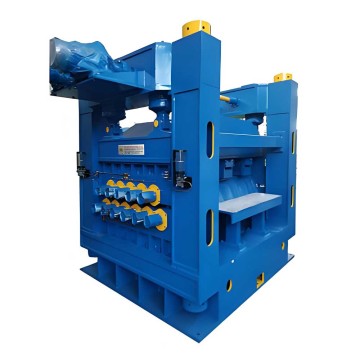
Professional Straightening Machine
Ultra-precise multi-roll configuration ensuring optimum linear tolerance prior to downstream stamping.
View Specifications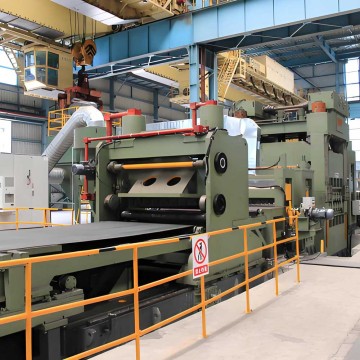
Hot Rolled Plate Moving Shear Line
Dynamic continuous flying cut line engineered for continuous high-speed strip severance without feed pausing.
View Specifications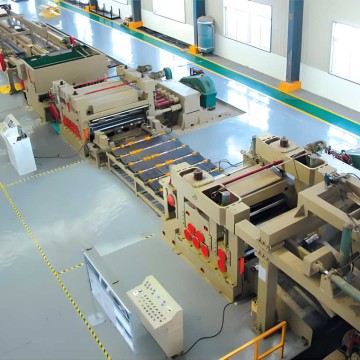
Stainless Steel Uncoiling-Shearing Line
Non-marking polyurethane roll system tailored for surface-sensitive stainless and polished aluminum coils.
View Specifications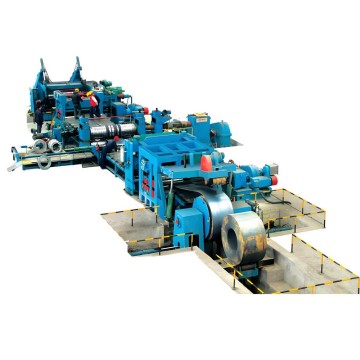
Combined Slitting & Cut-to-Length Line
Dual-capability manufacturing plant combining rotary longitudinal slitting and transverse shearing in one footprint.
View Specifications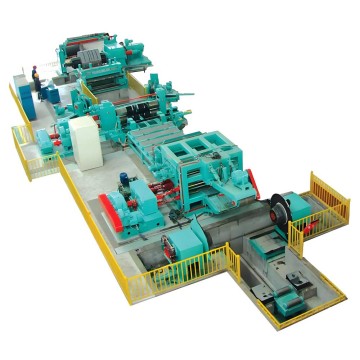
Uncoiling, Slitting & Recoiling Line
Heavy-duty rotary arbor slitter designed for heavy gauge processing with auto hydraulic scrap ballers.
View Specifications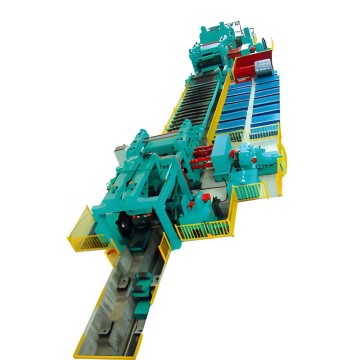
High-Speed Recoiling Slitter Line
Precision tension pad separation and differential recoiling shafts built for tightly packed strip packages.
View Specifications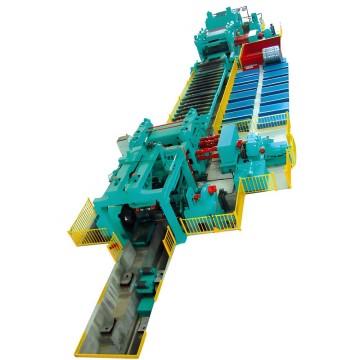
Automated Shearing & Stacking Line
High-precision pneumatic drop stacker and digital length control providing defect-free palletizing for export.
View SpecificationsThe Global Commercial & Industrial Status of Aluminum Slitting
Across modern metallurgy, the rapid acceleration toward lightweighting in e-mobility, aerospace structures, building facades, and lithium-ion battery packaging has elevated the aluminum slitter from basic workshop machinery into an ultra-precise, digitally calibrated production centerpiece.
The Lightweighting Mandate
With transport decarbonization targeting dramatic curb-weight reductions, global demand for 5xxx and 6xxx series aluminum coils has doubled over the past decade. Metal processing centers require slitters capable of handling variable ductility without scratching fragile conversion coatings.
Tension & Surface Integrity
Unlike high-strength carbon steel, non-ferrous aluminum strip is exceptionally susceptible to galling, edge rolling, and winding slippage. Leading aluminum slitter factories utilize multi-axis closed-loop tension systems to preserve micron-level flatness and strip stability.
Supply Chain Nearshoring
Global metal service centers in North America, Europe, and the Middle East are investing heavily in local master-coil processing hubs, reducing transit damage and tariff exposures by slitting locally on high-throughput, agile slitting lines.
Technological Roadmap & Evolution in Aluminum Slitter Engineering
From robotic tooling setups to real-time optical burr vision, the technological frontier for famous aluminum slitter manufacturers is anchored in reducing downtime, eliminating operator error, and meeting zero-defect quality standards.
Automated Knife Positioning
Automated robotic robotic arbor setup cuts tooling changeover from 45 minutes down to 3 minutes, calculating horizontal knife clearance and vertical overlap down to ±0.002 mm.
Non-Contact Laser Inspection
High-speed telecentric cameras continuously inspect slit edge geometry, flagging edge burr, camber anomalies, and edge tearing at line velocities up to 400 m/min.
Differential Tension Control
Pneumatically modulated friction segments ensure consistent winding torque on individual recoiler rings, compensating for natural gauge variations across wide master coils.
Cleanroom & Foil Slitting
Integrating dust extraction manifolds, enclosed cutting hoods, and static eliminators for high-purity aluminum foil (down to 6-12 microns) used in battery separators.
Wuxi Jianfa Engineering Philosophy: "Precision Is Governed by Stiffness"
Founded in the early 1980s and recognized as a national key developing enterprise in China's metallurgical machinery sector, Wuxi Jianfa builds heavy slitting line arbors from ultra-pure forged alloy steels (42CrMo), stabilized through deep cryogenic thermal cycling. This guarantees that arbors under dynamic radial and axial thrust experience deflection of less than 0.005 mm across the entire strip passline.
Localized Application Scenarios & Downstream Workflows
A world-class aluminum slitter factory does not supply standard machinery—it supplies tuned, alloy-specific manufacturing systems. Discover how our machines adapt to regional downstream sectors.
Automotive Outer Body Panels
Alloy grades such as AA6016 and AA5182 require zero-burr edge quality and completely scratch-free surfaces to avoid micro-stress cracks during hot deep drawing and stamp-forming operations.
Lithium Battery Enclosures & Foils
Slitting AA1060 and AA3003 down to thin strips for prismatic cell casings, cathode current collectors, and pouch tab leads where conductive particles or burs cause short circuits.
Architectural Facades & Roll Forming
Precision sizing for color-coated PVDF architectural coils, corrugated roofing sheets, composite honeycomb panels, and ducting where edge straightness prevents seam misalignment.
Macro Industrial Solutions: Machine Architecture Comparison
Selecting between specialized slitting, conventional cut to length (CTL), and synchronized flying shears requires balancing throughput demands against product geometry.
| Engineering Parameter | High-Precision Slitting Line | Heavy Cut to Length (CTL) Line | High-Speed Flying Shear Line |
|---|---|---|---|
| Primary Finished Form | Multiple continuous narrow coils | Individual flat sheets or thick plates | High-volume accurately sheared sheets |
| Strip Motion During Severance | Continuous high-speed rotary cut | Intermittent start-stop cycle | Continuous (flying synchronized carriage) |
| Typical Line Speed Range | 60 – 300 m/min | 20 – 80 m/min | 60 – 160 m/min |
| Key Core Mechanism | Double eccentric arbors, shimless spacers | 4-Hi or 6-Hi precision leveler + hydraulic shear | Servo planetary moving shear, optical encoder |
| Prime Industry Target | Tube mills, stamping plants, foil converters | Steel service centers, switchgear cabinets | Tier-1 auto blanking, high-tonnage sheet centers |
| Surface Protection System | Felt pads, PU rollers, air cushion belts | Rubberized entry rolls, non-marking drops | Magnetic or vacuum floating conveyor belts |
Why Wuxi Jianfa Stands Among Premier Slitting Factories
Building world-class metal processing machinery requires stringent in-house control over the entire production cycle—from CNC boring to electrical drive commissioning.
Complete Vertical Integration
We operate a 40,000 m² self-owned machine-building compound in Wuxi. Heavy gantry machining, gear milling, thermal quenching, and control cabinet builds occur completely under our roof.
40+ Years of Metallurgy
Operating since the early 1980s, our engineering team has designed more than 1,000 custom slitter configurations. We solve metal processing bottlenecks with deep engineering experience.
Rigorous Pre-Shipment Run
Prior to export packaging, lines undergo rigorous dry cycling and test strip slitting. Buyers are invited to our facility in Wuxi, Jiangsu to sign off on mechanical and electrical parameters.
Global Field Service
Our field engineers provide on-site foundation layout guidance, mechanical assembly, drive tuning, and local operator training in over 30 countries across 6 continents.
Frequently Asked Questions: Aluminum Slitter Engineering
Get straightforward answers from our senior metallurgists and commissioning teams on line specification, edge quality, tensioning, and export services.
What makes aluminum coil slitting technically different from carbon steel?
Aluminum features lower tensile strength but higher elasticity and galling affinity than steel. This requires specialized tungsten carbide or high-chrome D2 knives, precision ground spacers to avoid micro-burrs, polyurethane-coated guiding rolls to eliminate scratch marks, and sensitive closed-loop recoil tension control to prevent telescoping.
What thickness range and line speeds can Wuxi Jianfa lines process?
Our coil processing machinery encompasses ultra-thin aluminum foil and strip from 0.1 mm to heavy-gauge plates exceeding 16.0 mm. Processing speeds are matched to plant throughput: heavy plate lines run at 30-50 m/min, while high-efficiency thin strip slitting lines reach operational speeds up to 250-400 m/min.
How do you resolve winding discrepancies when slitting multiple strips?
Natural thickness variations across wide master coils cause slight outer diameter differences on the recoiler. We resolve this by integrating differential pneumatic friction shafts or individual tension stands equipped with variable-pressure felt pads, belt bridles, or non-marking polyurethane rolls that maintain uniform tightness across every strip.
What critical technical specifications are required for a customized quote?
To deliver an optimized engineering proposal, our team requires: material alloy grades and tensile/yield strength, incoming coil thickness and width, maximum coil weight and inner/outer diameter, minimum/maximum target slit strip widths, target output speed, and required factory electrical voltage/frequency specifications.
Do you deliver international on-site installation, commissioning, and training?
Yes. Wuxi Jianfa operates a dedicated international engineering service team. We deploy mechanical and PLC commissioning engineers directly to your facility overseas to oversee foundation positioning, equipment alignment, electrical wiring, trial coil commissioning, and hands-on maintenance crew training.
Can international buyers inspect machinery in Wuxi prior to shipment?
Absolutely. We encourage on-site pre-shipment FAT (Factory Acceptance Testing). Our 40,000 m² factory is located in Wuxi, Jiangsu Province, directly connected by high-speed rail to Shanghai. Clients can inspect machining tolerances, review component certifications, and observe full operational cycling before overseas dispatch.
Explore Our Full Range of Metal Processing Solutions
Review our high-performance coil slitting, cutting, leveling, and shearing systems. Every line can be custom-engineered to meet your mill's exact space, tonnage, and tolerance requirements.
High Strength Leveling Machine
Heavy structural multi-roll leveler designed to deliver high flatness in yield-intensive alloy coils.
Explore Machine
Professional Straightening Machine
Calibrated straightening arbor rolls built for precision strip feeding into cold-forming processes.
Explore Machine
Hot Rolled Plate Moving Shear Line
Continuous cutting-on-the-fly system engineered for high productivity in sheet service centers.
Explore Machine
Stainless Steel Cut-to-Length Stacker
Specialized surface protection mechanics preventing friction scratches on decorative coils.
Explore Machine
Combined Slitting & CTL Line
Versatile production line allowing seamless switching between slitting and high-speed precision cut-to-length.
Explore Machine
Industrial Slitting & Recoiling Line
Designed for heavy duty operations with rigid cutter stands and quick-change cutter head cars.
Explore Machine
High-Efficiency Strip Slitting Unit
High-precision recoiling system with hydraulic push-off plates and automated turnstiles.
Explore Machine
Integrated Shearing & Stacking Plant
High-speed magnetic/air-cushioned sheet stacker with integrated weight inspection sensors.
Explore Machine