High-Precision Metal Processing Lines & Slitters
Direct factory engineered solutions meeting international tolerances for hot-rolled, cold-rolled, galvanized, stainless steel, and automotive aluminum processing.








Wuxi Jianfa Machine-Building: Proven Industrial Pedigree
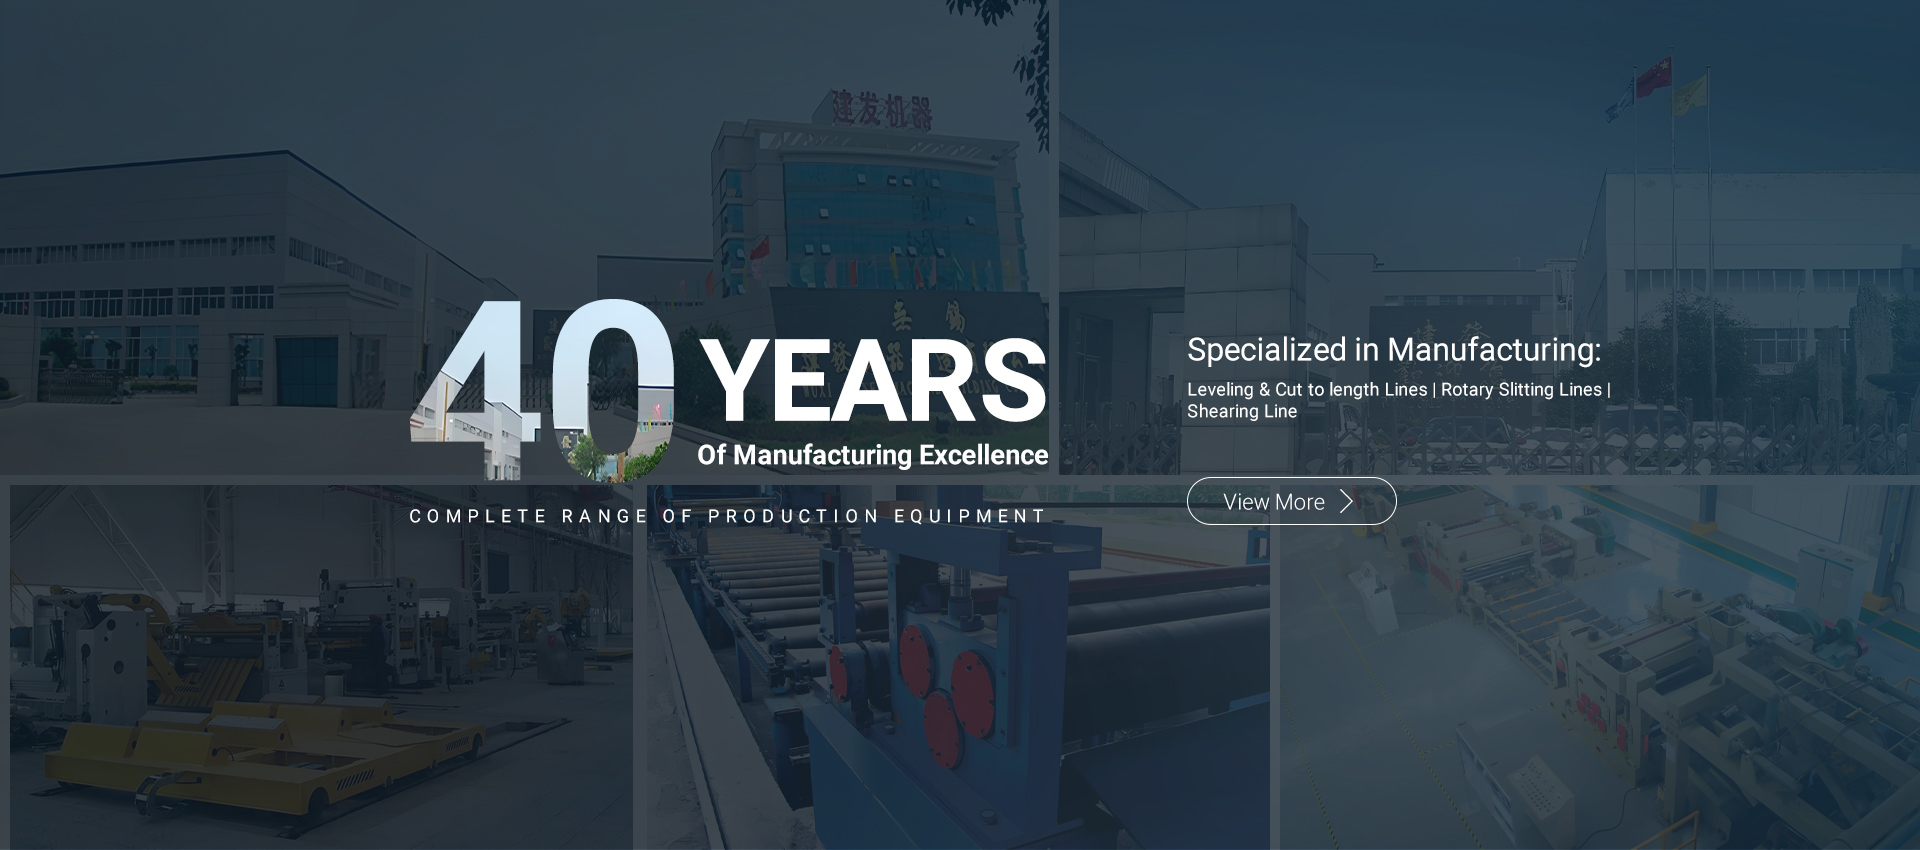
Since our founding in the early 1980s, Wuxi Jianfa has continuously evolved into a national key developing enterprise in China's metallurgical machinery sector. Operating from a fully equipped modern heavy-industrial facility, we engineer and construct high-durability production lines under strict ISO standards.
Refining high-speed shearing and precision slitting geometry since 1980s.
Dedicated heavy machining, horizontal boring, thermal treatment & QA test bays.
Substantial balance sheet guaranteeing long-cycle turnkey steel processing lines.
Metallurgical specialists, PLC developers, hydraulic techs, and field engineers.
Monolithic Arbor & Base Rigidity
Every slitter head utilizes normalized, stress-relieved high-tensile cast frames. Heavy alloy arbors ground to ultra-precision sub-micron radial tolerances minimize dynamic runout, preventing edge burrs even during extreme speed transitions.
Siemens & Rexroth Automation
Integrated motion logic controls strip tracking, dynamic loop depth, hydraulic back-tensioning, and speed synchronization between the pay-off uncoiler, slitter arbor, tension bridle, and recoiler drums for zero slippage.
Full In-House QA Protocol
From metallurgical ultrasonic non-destructive testing (NDT) on raw steel plates to laser-interferometer alignment of roll axes, our machines leave our Wuxi factory only after passing continuous load testing.
China's Industrial Ecosystem: Unmatched Scale & Cost Efficiency
Procuring metal processing machinery directly from our manufacturing facility in Wuxi, Jiangsu offers distinct operational, economic, and logistical advantages for international steel fabricators and service centers.
Yangtze River Delta Cluster
Located in the heart of China's heavy precision manufacturing belt, our Wuxi facility benefits from immediate access to top-tier steel foundries, advanced tooling suppliers, and specialized heat treatment facilities, drastically slashing lead times.
30–45% Capex Optimization
Compared to European or North American equipment builders, Jianfa provides identical high-grade international components (SKF, Rexroth, Siemens, Schneider) at a fraction of the total system capex, delivering payback periods under 18 months.
Direct Deep-Water Port Logistics
With direct arterial expressway connection to Shanghai Port and Taicang Port, large monolithic machine bases and breakbulk line assemblies transition smoothly from factory floor to container vessel with zero overland transit delay.
Engineering Standards: Slitting Line vs Cut-To-Length vs Flying Shear
International procurement teams require exact metallurgical matching. Review our engineering selection parameters before defining your line capacity.
| Evaluation Parameter | High-Speed Slitting Line | Standard Cut-To-Length (CTL) | Synchronized Flying Shear Line |
|---|---|---|---|
| Primary End-Product | Multi-strand narrow strips on tight recoil drums | Flat dimensioned sheets, squared & stacked | Continuous flat plates cut without halting strip |
| Strip Gauge Capability | 0.2 mm to 16.0 mm (Mild, Stainless, High-Yield) | 0.5 mm to 25.0 mm heavy plate | 1.0 mm to 14.0 mm plate & sheet |
| Line Speed Range | Up to 200 m/min (Variable speed vector drive) | 30 – 80 m/min (Start-stop measuring roll) | Up to 120 m/min (High continuous throughput) |
| Shear Kinematics | Dual-head rotary slitter with scrap choppers | Hydraulic down-cut / mechanical guillotine shear | Servo-driven crank or rack traveling carriage |
| Target Industrial Users | Tube & pipe mills, stamping, roll formers | Steel service centers, automotive blanking | Heavy shipbuilding, structural construction panels |
| Downstream Process | Coil banding, strapping & automated turnstiles | Pneumatic/magnetic drop stackers & palletizers | Continuous automated conveyor packaging |
Localized Support, CE Compliance & Operational Safety
Deploying heavy equipment into modern factories requires strict adherence to international electrical, mechanical, and operator workplace safety standards.
CE Machine Safety Directive
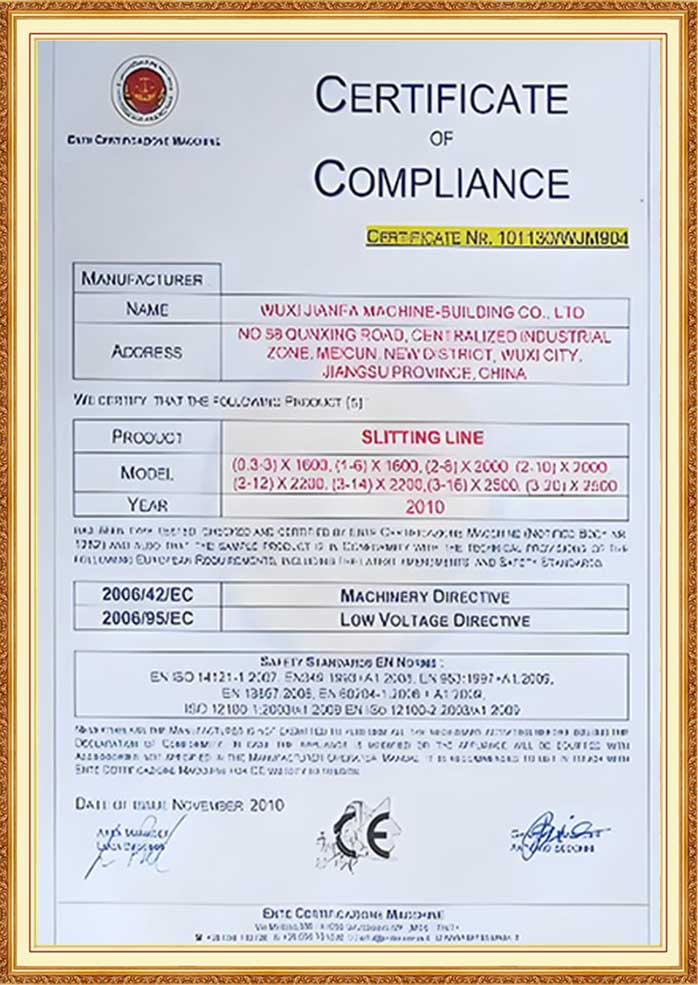
Lines are compliant with EU 2006/42/EC directives, incorporating interlocked light curtains, perimeter safety fences, dual-channel emergency stop circuits (Cat. 4 / PL e), and hydraulic anti-drop valves.
UL / CSA Electrical Cabinets
For North American clients, we build custom electrical control suites conforming to NFPA 79 and UL 508A specifications, using certified wire conduits, short-circuit current ratings (SCCR), and NEMA enclosures.
Global Field Engineering (FSE)
Our multilingual commissioning engineers arrive on-site across Europe, North America, Southeast Asia, and the Middle East for foundation leveling, electrical loop testing, trial slitting, and comprehensive operator training.
Emerging Industry Trends in Coil Processing Machinery
The global coil slitting market is undergoing rapid transformation driven by lightweight automotive materials, higher steel yield strengths, and Industry 4.0 connectivity.
AHSS & Ultra-High Strength Steels
Processing advanced high-strength steels (DP980, DP1180, Martensitic grades) requires heavy arbor torque ratings, specialized tungsten-carbide knives, and rigid backup roll clusters to prevent arbor deflection and strip edge fracture.
Automated Robotic Knife Setup
To reduce setup downtime between slitting orders, modern lines integrate robotic tool changers or quick-change twin-turret slitter heads that allow off-line knife stacking in under 3 minutes while the line is running.
IoT Edge Diagnostics & Telemetry
Equipped with encrypted VPN gateways, our lines stream vibration data, bearing temperatures, motor torque spectra, and hydraulic pressure cycles directly to cloud predictive maintenance modules for real-time fault prevention.
Localized Applications: From Automotive Stamping to Heavy Infrastructure
Engineered to adapt to sector-specific metallurgical specifications across global industrial clusters.
Automotive Body-in-White (BIW)
Processing delicate aluminum (5000/6000 series) and exposed outer-body panels requires non-marking PU-coated tension rolls, vacuum sheet stackers, and zero-camber slitting tolerances to safeguard pristine surface cosmetics.
ERW Tube & Structural Pipe Mills
Supplying continuous high-speed strip uncoiling to tube mills requires burr-free edge trim, uniform slit edge elongation, and tight pancake recoiling for uninterrupted welding line feed.
Transformer Core & Electrical Steel
High-grade Grain-Oriented Silicon Steel (CRGO) processing demands ultra-precise micro-slitting with carbide knives maintaining burr heights strictly under 0.01 mm to eliminate magnetic eddy current losses in core assemblies.
Recognized Quality Systems & Verified Certifications
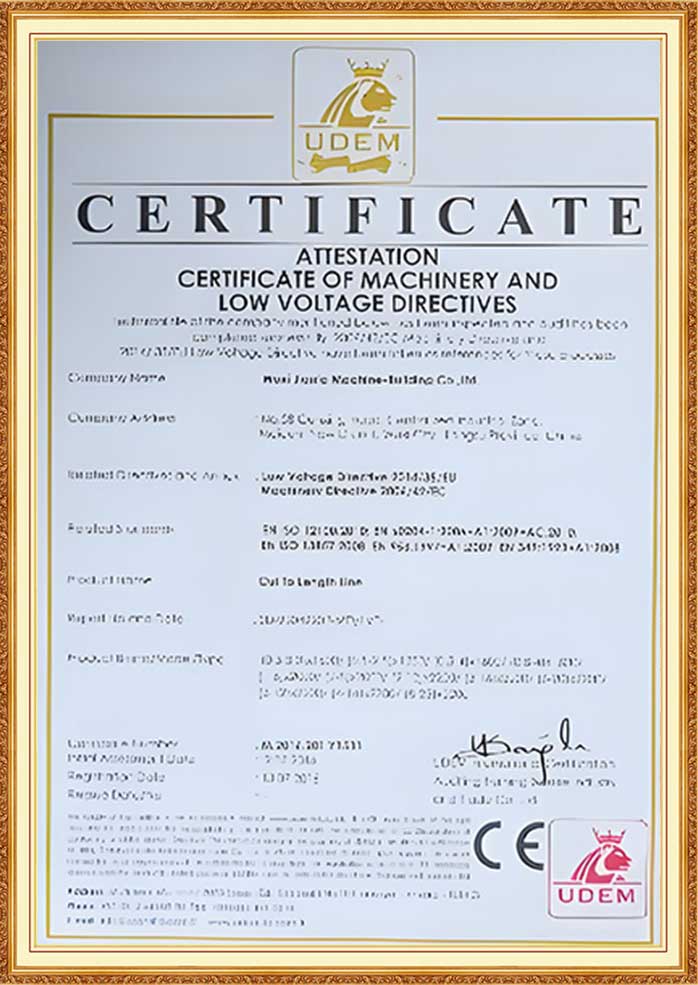
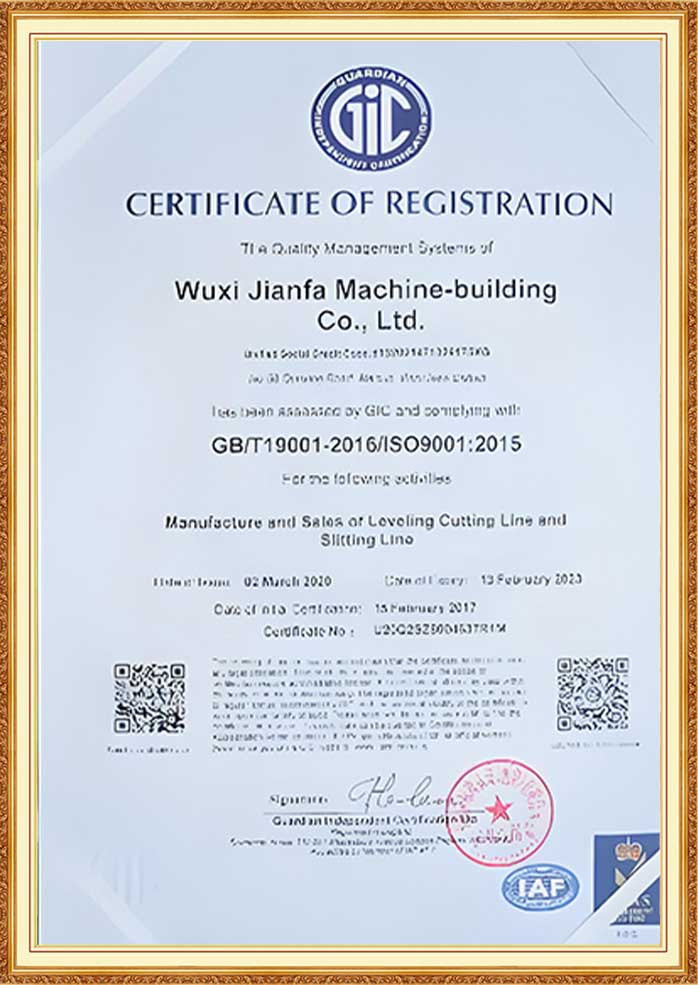
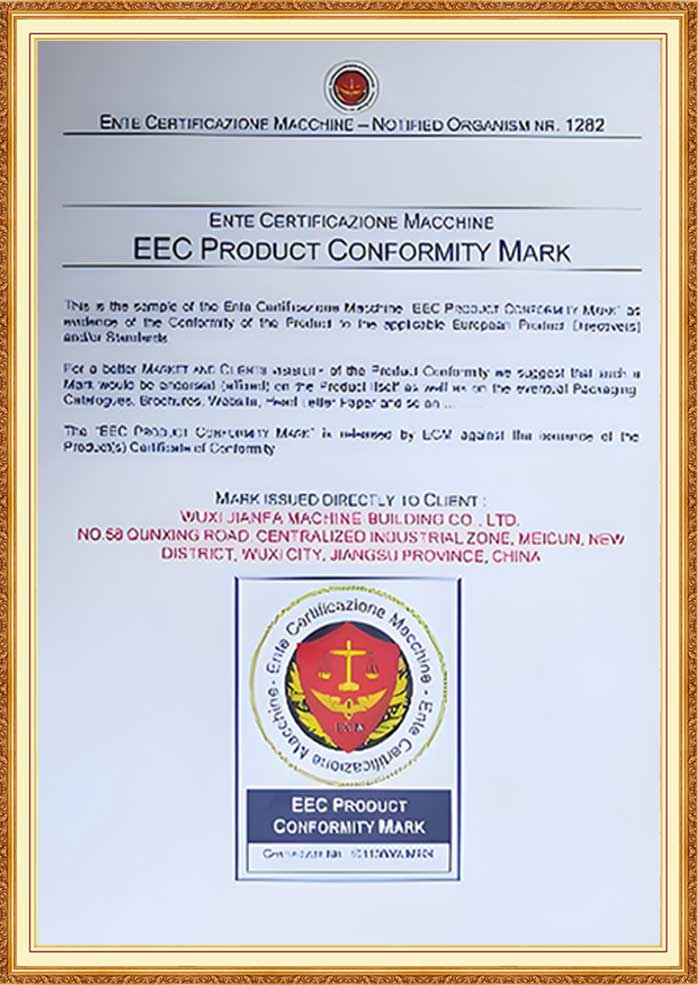
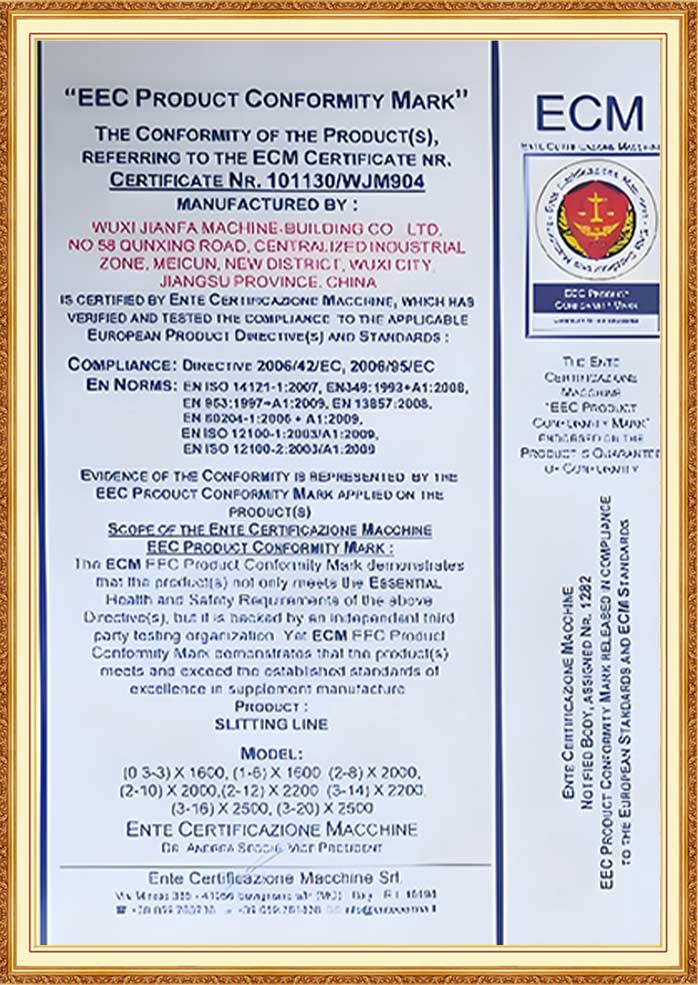
“Sincerity can open even the hardest stone.” Jianfa guarantees audited factory compliance, documented metallurgical heat records, and third-party inspection verification.
Practical Technical Insights from Our Plant Engineers
Proven operational guidelines addressing common field commissioning and maintenance challenges.
Commissioning Protocols Before New Slitter Start-Up
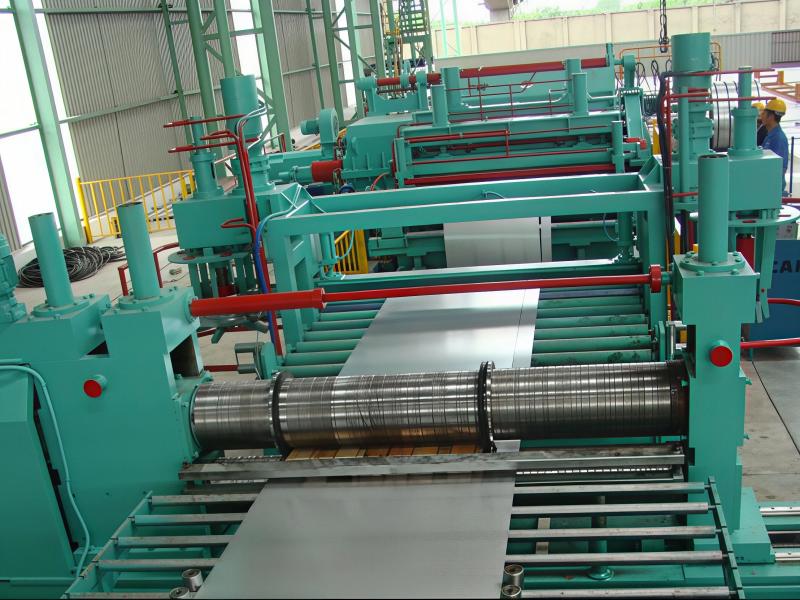
A new slitting line must undergo systematic alignment of the uncoiler drum, hydraulic arbor parallelism calibration, and knife horizontal clearance testing before full load production.
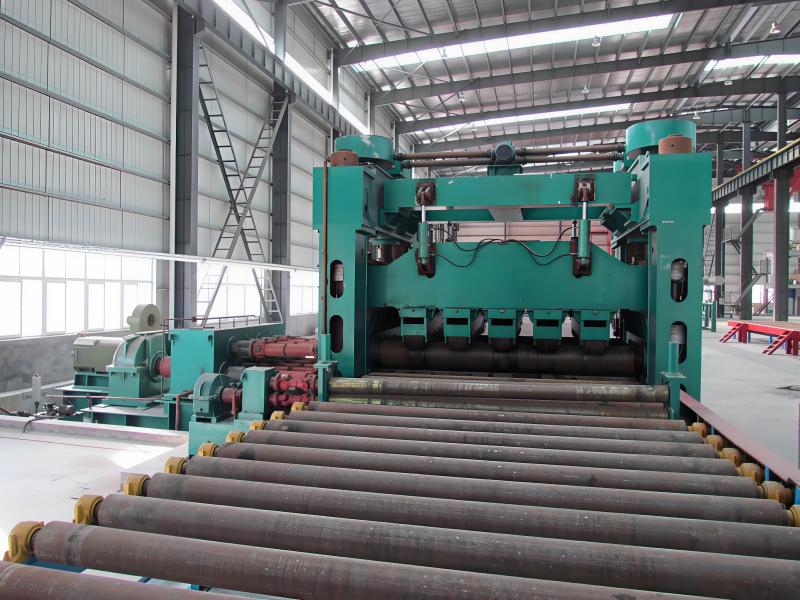
Mastering CNC Leveling Machine Parameter Controls
Understanding how back-tension, roll intermesh, and intermediate counter-bending rolls eliminate center buckle, camber, and coil set on modern graphical HMI operator interfaces.
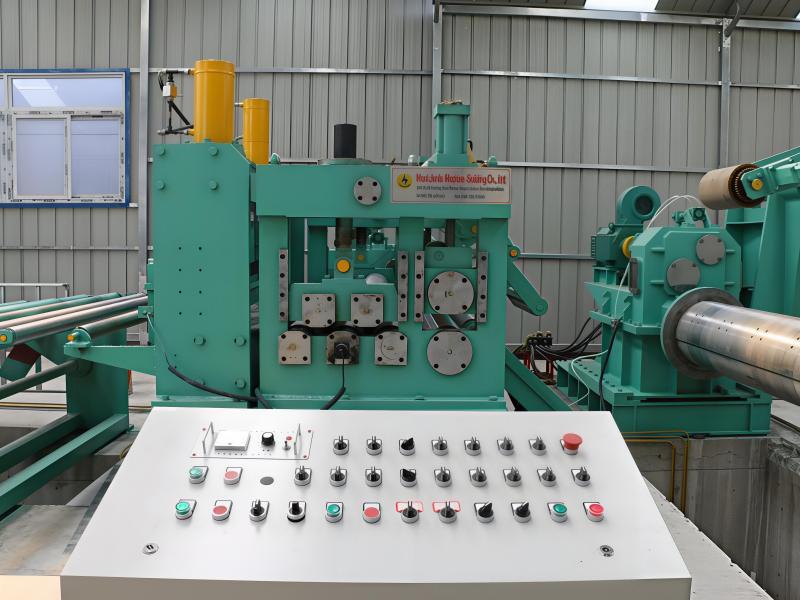
Automatic vs. Semi-Automatic Slitting Line Efficiency
Detailed cost-benefit analysis comparing automated coil loading cars, automatic scrap baling, and quick-change cutter heads against conventional semi-manual configurations.
Frequently Asked Questions by Global Procurement Engineers
Comprehensive answers regarding machine capacities, component sourcing, international commissioning, and custom engineering.
What coil processing equipment does Wuxi Jianfa manufacture?
We manufacture complete turn-key coil processing lines including precision rotary slitting lines, heavy-gauge cut-to-length (CTL) lines, high-speed flying shear lines, multi-roller leveling machines, four-high/six-high straightening systems, and integrated continuous galvanizing production lines. Equipment can be supplied as a complete greenfield installation or as modular standalone units to retrofit existing lines.
Which materials and tensile ranges can your slitting and CTL lines process?
Our processing lines handle hot-rolled carbon steel, cold-rolled coils, galvanized (GI/GL), pre-painted steel (PPGI), stainless steel (200, 300, 400 series), silicon electrical steel, and automotive aluminum alloys. We configure specialized heavy-torque lines capable of slitting and leveling advanced high-strength steels (AHSS) with yield strengths exceeding 1200 MPa.
How do I determine whether my plant requires a Slitting Line, CTL Line, or Flying Shear?
Choose a Slitting Line when the target product is narrow continuous coiled strips for tube mills, roll-forming, or progressive die stamping. Choose a Cut-To-Length Line when producing stacked, dimensioned flat sheets or thick plates where edge squaring is critical. Choose a Flying Shear Line when ultra-high sheet output is required, as the shear mechanism accelerates and synchronizes with strip motion to cut continuously without stopping the feeder.
What parameters are required to generate an accurate technical & commercial quotation?
Please provide: 1) Material type and yield strength (MPa); 2) Coil thickness range (min/max mm) and width (mm); 3) Maximum parent coil weight and inner/outer diameters; 4) Target slitting count and minimum slit width, or target sheet cut lengths; 5) Tolerance criteria (width tolerance, camber, diagonal squareness); and 6) Target speed (m/min) and local plant electric power supply (V/Hz/Ph).
How do you handle overseas field installation, commissioning, and training?
We dispatch dedicated mechanical and electrical commissioning engineers to your plant to oversee foundation anchoring, mechanical alignment, hydraulic piping interconnection, and PLC debugging. Our team conducts full operator training covering knife setup calculations, line safety protocols, and routine maintenance before project sign-off, supported continuously by 24/7 remote diagnostic telemetry.
Can buyers visit the Wuxi manufacturing facility to perform Factory Acceptance Testing (FAT)?
Yes, absolutely. We welcome and encourage comprehensive on-site Factory Acceptance Testing (FAT) at our 40,000 m² Wuxi facility, located just 30 minutes from Shanghai via high-speed rail. Buyers or their designated third-party inspection agencies (SGS, TÜV, Bureau Veritas) can inspect raw component machining, verify dimensional tolerances, and observe complete running dry-cycle and coil-loading trials prior to seaworthy packing.
Engineered Coil Processing Systems Ready for Deployment
Explore our complete catalog of certified slitting, moving shear, and automated sheet leveling solutions.