
Primary Industrial Coil Processing Equipment
Explore our heavy-duty rotary shear slitting lines, automated cut-to-length systems, and flying shears designed for extreme dimensional stability and continuous production uptime.

High-Quality Professional Flying Shear Line
Non-stop continuous synchronization shear for high-volume coil processing with minimal cycle latency.

CE Certified Heavy Cut to Length Line
Multi-roller precision leveling and shearing with absolute sheet flatness and zero surface marring.

Automated Precision Steel Slitting Line
Engineered for high-yield steel coil strip division, tight arbor tolerance, and smooth edge winding.

High Strength Multi-Roll Leveling Machine
Eliminates internal stress and residual coil camber across high-tensile hot rolled steel alloys.

Professional Heavy Straightening Machine
Specialized hydraulic backup rolls ensuring flat, warp-free plates for downstream stamping operations.

Hot Rolled Plate Moving Shear System
High-torque dynamic tracking shear mechanism for heavy gauge hot-rolled strips without stopping.

Stainless Steel Cut-to-Length & Stacker
Polyurethane coated pinch rolls and vacuum drop stackers dedicated to 2B/BA finish protection.

Combined Coil Slitting & CTL Line
Integrated space-saving layout executing both longitudinal slitting and cross-shearing in one pass.
Integrated CNC In-House Machining
Every heavy arbor, bearing pedestal, leveling roll, and recoiler drum is fabricated, normalized, precision turned, and cylindrical ground in our Wuxi machine shop to guarantee runout tolerances below 0.005mm.
Advanced Metallurgical Line Controls
Equipped with Siemens, Mitsubishi, or Schneider PLC platforms, closed-loop servo drives, and synchronized line velocity management up to 300 m/min, assuring zero coil slippage and tension-consistent winding.
Factory Direct Accountability
Wuxi Jianfa eliminates agent layers. From initial Finite Element Analysis (FEA) on structural slitter frames to overseas wet-commissioning and lifelong spare parts dispatch, buyers interface directly with OEM engineers.
Anatomy of a High-Precision Automatic Slitting Line
A comprehensive engineering review of how Wuxi Jianfa integrates modular sub-assemblies to achieve micron-level strip accuracy, burr minimization, and continuous high-speed strip tracking.
1. Entry Coil Management
Heavy-duty hydraulic coil loading cars, single or double-mandrel decoilers with pneumatic/hydraulic disc brakes, and automatic wedge expansion ensuring secure centering of master coils up to 35,000 kg.
2. Dual Slitter Head Turret
Allows rapid tooling offline while the active head runs. Hardened forged alloy arbors (42CrMo/SCM440) supported by ultra-precise Timken/SKF double-row tapered bearings eliminate dynamic arbor deflection.
3. Looping Pit & Tension Unit
Accommodates material thickness variations across the strip profile. Belt-bridle, felt-friction, or pneumatic roller tension stations apply calibrated back-tension without scuffing delicate metal coatings.
4. Recoiler & Turnstile
Seamless hydraulic expansion recoilers with overarm push-off arms, strip separators, and 4-arm turnstiles facilitating high-efficiency offloading, strapping, and immediate transition to secondary packing lines.
Technical Roadmap & Future Outlook: The Smart Slitting Paradigm
The transition from conventional mechanical slitting to fully autonomous Industry 4.0 coil processing platforms requires breakthroughs in servo automation, optical inspection, and adaptive tension dynamics.
Automated Robotic Knife Setup
Eliminating manual shimming errors. Jianfa is piloting linear encoder-driven servo tooling robots that configure male/female slitting rotary blades, rubber stripper rings, and spacers with ±0.002mm repeatability in under 3 minutes.
In-Line AI Vision Defect Scanning
High-resolution telecentric line-scan cameras integrated immediately downstream of the rotary slitter detect edge burrs, camber distortions, and surface slivers in real-time, tagging defective strips before recoiling.
Cloud Telemetry & Predictive Maintenance
Built-in OPC-UA/MQTT protocols stream arbor vibration harmonics, hydraulic oil thermal signatures, and drive torque metrics to centralized SCADA systems, preventing catastrophic bearing failure and unscheduled line downtime.
Macro Industry Solutions: Engineered for Demanding Alloys
Different metals manifest distinct shear yield curves, work hardening indices, and surface friction behaviors. Jianfa customizes slitting knife clearances, drive kinematics, and recoiling tension curves accordingly.
Automotive AHSS & UHSS
Processing advanced high-strength steels (DP980, QP1180, Martensitic steels) up to 1500 MPa tensile strength with oversized forged arbors, high-clearance carbide blades, and rigid zero-backlash drives.
CRGO/CRNGO Electrical Steels
For transformer cores and EV e-motors. Requires ultra-low burr performance (<0.01mm) to prevent interlaminar eddy-current losses. We implement tungsten carbide knives and diamond-ground spacers.
Stainless Steel (300/400 Series)
Addressing strong work-hardening characteristics and strict surface aesthetics. Incorporates non-marking polyurethane contact rolls, PVC paper interleaving uncoilers, and dual-action scrap winders.
Aluminum & Copper Foils
Ultra-thin slitting lines for lithium-ion battery cathode/anode current collectors and architectural facades. Featuring precision micro-gap adjustment, active web guiding (EPC/CPC), and soft tension control.
China Factory 4.0: Supply Chain Resilience & Efficiency
Wuxi Jianfa combines the dense industrial manufacturing ecosystem of the Yangtze River Delta with European-grade dimensional tolerances, delivering unprecedented TCO value to international steel processors.
Strategic Delta Logistics Hub
Situated in Meicun Industrial Zone, Wuxi, Jiangsu, with direct heavy highway connections to the Port of Shanghai. Facilitates oversized containerization (OT/FR racks) and ensures rapid sea-freight dispatch worldwide.
100% Vertical Component Integrity
We do not outsource critical structures. Heavy welded frames undergo shot blasting and thermal stress-relieving annealing furnaces before machining on our large-scale floor-type boring and milling machining centers.
35-45% TCO Reduction
Procuring factory-direct from Jianfa saves international steel service centers up to 45% in capital expenditure compared to traditional Italian or German OEM counterparts, while delivering identical metallurgical strip tolerances.
Global Enterprise Technical Evaluation Matrix
When compiling equipment RFPs for slitting lines, cut-to-length systems, or high-speed flying shears, procurement directors should benchmark against these standardized engineering parameters.
| Evaluation Parameter | Light-Gauge Slitting Line | Heavy-Gauge Plate Slitting Line | Flying Shear CTL Line |
|---|---|---|---|
| Strip Thickness Range | 0.15 mm – 3.0 mm | 3.0 mm – 16.0 mm (Up to 25mm Hot Rolled) | 0.5 mm – 6.0 mm |
| Coil Width Capacity | 600 mm – 1650 mm | 1000 mm – 2200 mm | 800 mm – 2000 mm |
| Line Velocity | Up to 250 – 300 m/min | Up to 60 – 100 m/min | Up to 80 – 120 cuts/min (Continuous) |
| Slit Width Tolerance | ±0.02 mm to ±0.05 mm | ±0.10 mm to ±0.20 mm | Length Tolerance: ±0.3 mm / 2000mm |
| Burr Ratio Limit | ≤ 3% of material thickness | ≤ 5% of material thickness | Clean 90° cut, no edge roll-over |
| Arbor Runout Precision | Radial ≤ 0.005mm; Axial ≤ 0.005mm | Radial ≤ 0.008mm; Axial ≤ 0.008mm | Synchronized servo carriage track |
| Tooling Changeover Time | < 5 min (Dual head turret with quick disconnect) | < 15 min (Hydraulic arbor locking) | Tool-free touchscreen length presets |
Localized Support & International Compliance Assurance
Operating in 30+ countries mandates unwavering adherence to regional industrial safety standards, robust electrical architectures, and responsive technical field teams.
CE & OSHA Safety Standards
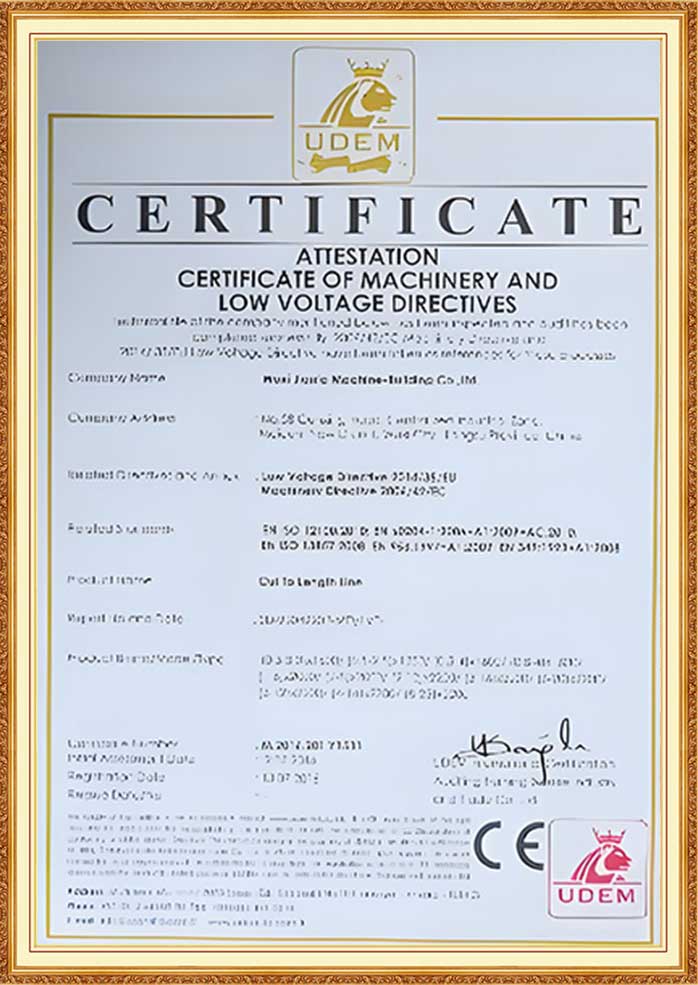
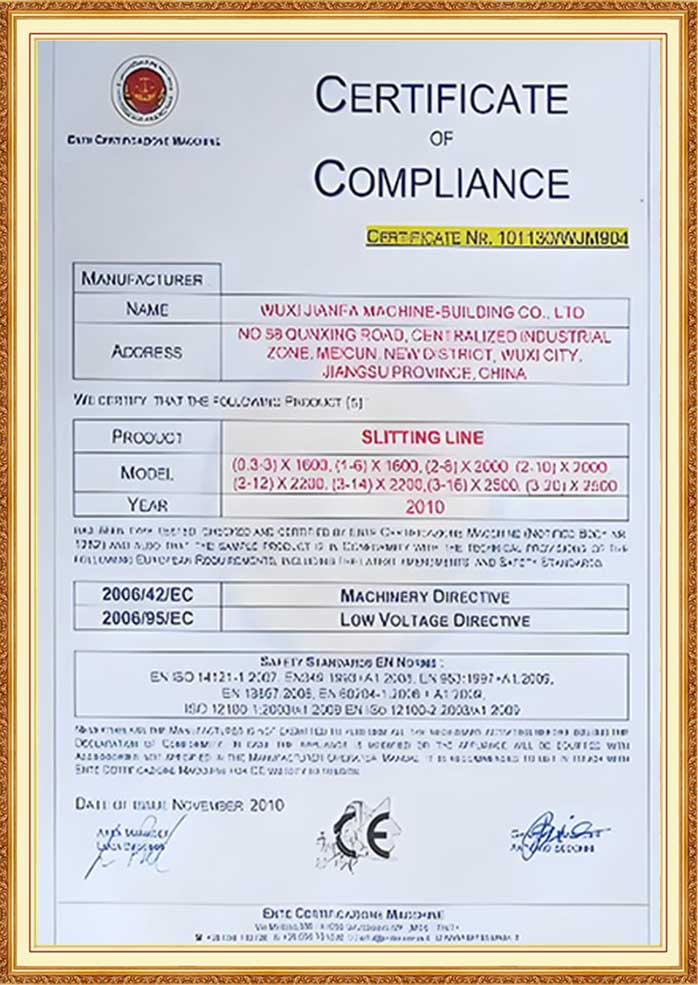
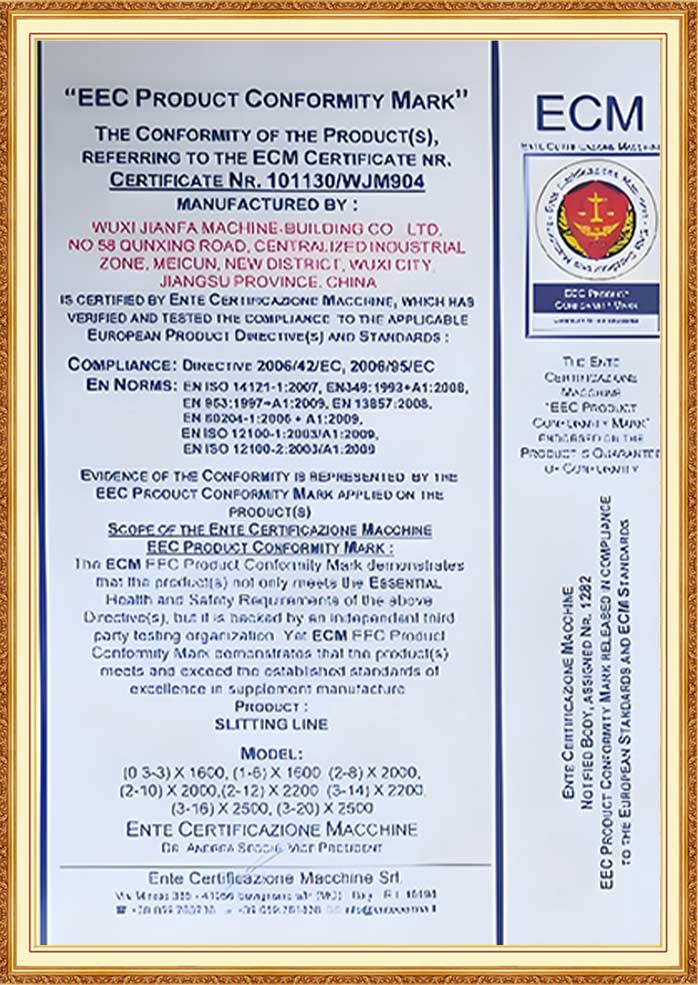
Fully compliant with EU Machinery Directive 2006/42/EC, EN ISO 12100, EN 60204-1, and American OSHA requirements. Features physical perimeter light curtains, Category 4 safety interlocks, and redundant hydraulic shut-offs.
Bilingual Commissioning Engineers
Our experienced mechanical and electrical commissioning engineers travel directly to overseas client facilities across the USA, Mexico, Brazil, Saudi Arabia, UAE, and Southeast Asia to oversee foundation anchoring, wiring, and trial runs.
72-Hour Rapid Spares Dispatch
We maintain an exhaustive strategic inventory of critical wear components—including spare hydraulic valves, circular shear blades, stripper rings, and encoders—guaranteeing expedited international courier dispatch within 48 to 72 hours.
OEM Factory Qualifications & Accreditations
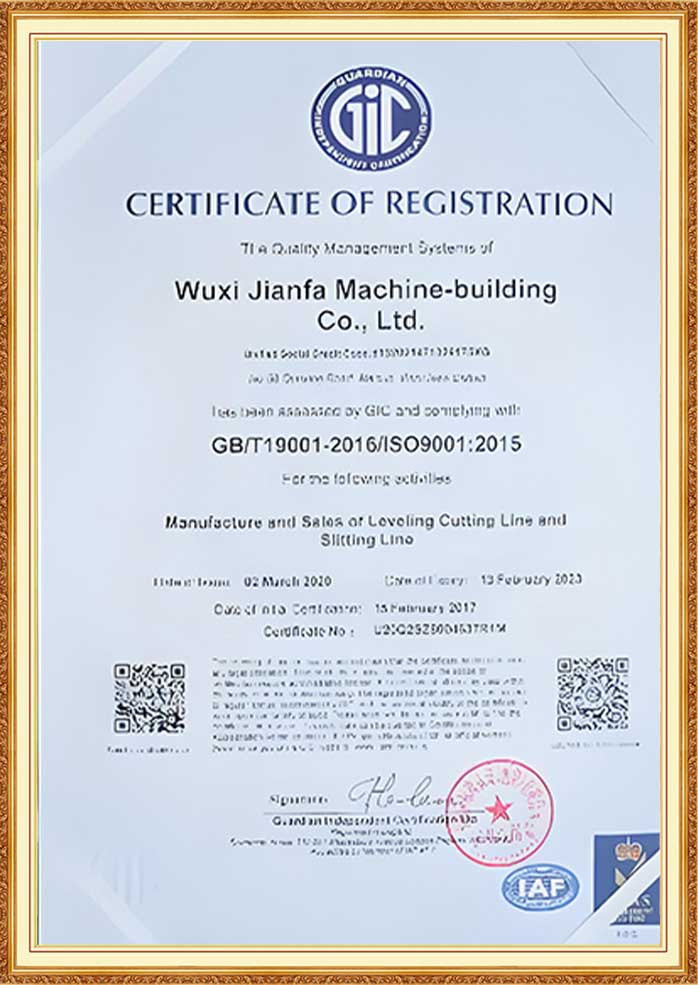
Four decades of metallurgical manufacturing discipline documented through authentic state and international quality recognitions. Factory audits and pre-shipment FAT tests are cordially welcomed.
Frequently Asked Questions: Slitting Engineering
Direct technical answers from Wuxi Jianfa senior application engineers on precision knife setup, tension management, material tolerances, and international commissioning.
How does Wuxi Jianfa guarantee minimum strip edge burr during high-speed slitting?
Edge burr control depends on arbor rigidity and accurate knife horizontal clearance. Our slitter arbors are machined from 42CrMo high-alloy forgings, tempered, and precision ground with bearing runout ≤ 0.005mm. Combined with custom shimless tooling and calibrated rubber stripper rings, edge burr is maintained consistently below 3% of strip thickness.
What is the mechanical advantage of a Dual-Head Turret Slitter?
A dual-head turret enables offline tooling setup. While head "A" is actively slitting coils, operators assemble knives and spacers on head "B" using ergonomic tooling arms. Head rotation takes under 2 minutes via hydraulic pivot pins, shrinking line changeover downtime from 45 minutes down to under 5 minutes, significantly elevating Overall Equipment Effectiveness (OEE).
How does the tension unit handle differential strip thicknesses from crowned master coils?
Master coils typically exhibit a convex crown where the center gauge is thicker than the edges. If recoiled under uniform tension, edge strips sag while center strips wind overly tight. We implement multi-zone looping pits combined with pneumatic felt-pad tension stations or individual friction-ring belt bridles, ensuring uniform recoil tightness across all slit coils.
Which coil parameters are essential to generate a binding technical quotation?
Please furnish: (1) Material grade & yield strength (MPa), (2) Strip thickness range (min/max mm), (3) Master coil width and max weight (metric tons), (4) Number of slit cuts required per gauge, (5) Coil inner/outer diameter (ID/OD), and (6) Available industrial line power (voltage/frequency) and factory bay dimensions.
Can your slitting and cut-to-length lines be equipped for surface-critical materials?
Yes. For stainless steel (BA/No.4 finish) and automotive skin-pass aluminum coils, all conveyor rolls, bridle rolls, and leveling cylinders are coated with anti-scratch polyurethane or chrome-plated with mirror polishing (Ra ≤ 0.05μm). Additionally, our lines can integrate top and bottom protective film laminators with synchronized edge trimmers.
What is the expected delivery timeframe and commissioning protocol?
Standard lead time ranges from 90 to 150 days depending on coil thickness capacity and line complexity. Every machine undergoes a comprehensive dry and wet Factory Acceptance Test (FAT) at our Wuxi facility before containerization. Our field engineers arrive on-site for line positioning, laser leveling, wiring inspection, hydraulic pressure tests, and operator certification.
High-Performance Coil Processing Machinery
Engineered for high-volume metal processing service centers, tube and pipe producers, stamping facilities, and electrical core manufacturers worldwide.
High Strength Leveling Machine
Engineered with multi-roll cassettes to eliminate coil curvature and internal stress in high-yield alloys.
Professional Straightening Machine
High-precision intermediate backup rolls to correct center buckle and edge waves in thick metal sheets.
Hot Rolled Plate Moving Shear Line
Continuous dynamic shearing designed for heavy plate service centers requiring maximum sheet output.
Stainless Coil CTL & Stacker Line
Designed with specialized air-cushion stackers to ensure zero scratches on high-finish decorative sheets.
All-in-One Slitting & CTL Line
Uncoiling, longitudinal slitting, leveling, precision shearing, and automatic pallet stacking in one station.

HR Sheet Slitting & Recoiling Line
High-torque slitter arbors and robust scrap winders engineered specifically for thick-walled hot rolled coils.

HR Uncoiling-Slitting-Recoiling Line
Reliable narrow strip supply line feeding high-frequency ERW pipe mills and structural roll formers.

HR Uncoiling-Leveling-Shearing Line
Automated heavy sheet processing with high-speed pneumatic drop stackers and automatic strapping.
Build Your Custom Coil Processing Line With Factory Engineers
Bypass agents and traders. Discuss your material specs, desired line speed, and factory floor plan directly with the senior engineering team at Wuxi Jianfa Machine-Building Co., Ltd.