
State-of-the-Art Cold Rolled Processing Equipment
Engineered for cold-rolled carbon steel, silicon sheets, stainless steel, and automotive-grade alloys with guaranteed edge tolerance and maximum uptime.
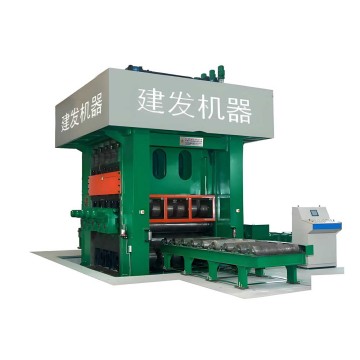
High Strength Leveling Machine
Multi-roll roller leveler removing residual stress, edge waves, and center buckles for high-yield steel coils.
View Specification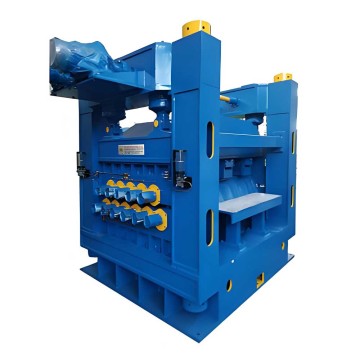
Professional Straightening Machine
Calibrated mechanical straightening units ensuring absolute strip flatness prior to precision blanking operations.
View Specification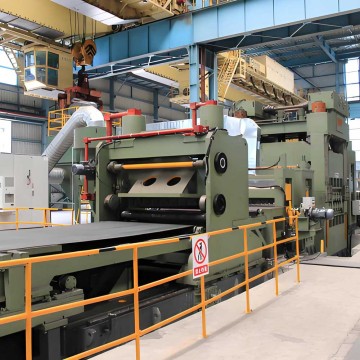
Hot Rolled Plate Moving Shear Line
High-throughput synchronized shear systems designed for dynamic cut-to-length tasks without stopping the strip line.
View Specification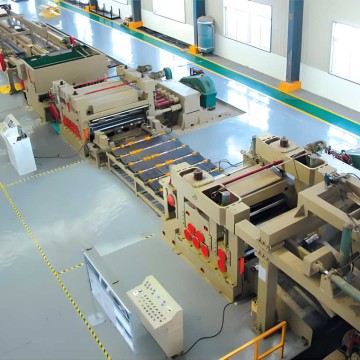
Stainless Steel Shearing & Stacking Line
Zero-mar uncoiling, dynamic leveling, and magnetic/air-cushioned automated stacking for 2B, BA, and No.4 finish surfaces.
View Specification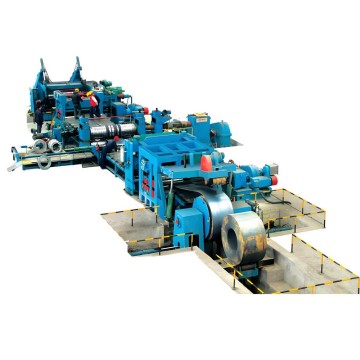
Combined Slitting & CTL Line
Integrated multi-mode architecture providing simultaneous slitting, precision leveling, cut-to-length, and sorting.
View Specification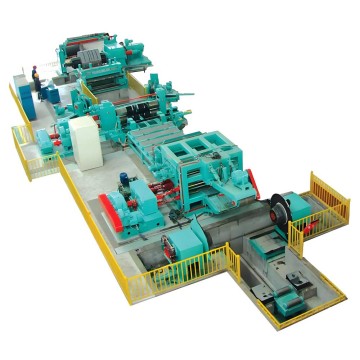
Sheet Slitting & Recoiling Line
High-rigidity arbor slitter housing with quick-change tooling turnstiles and synchronized dynamic tension stands.
View Specification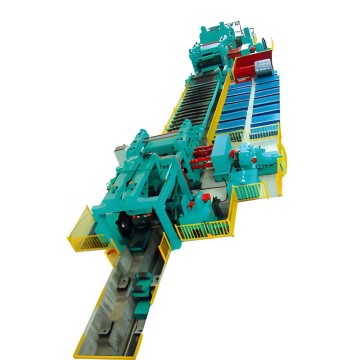
Heavy Duty Slitting & Recoiling Line
Engineered for high-yield tube mills, structural profiles, and thick metal edge trimming with heavy dual-mandrel uncoilers.
View Specification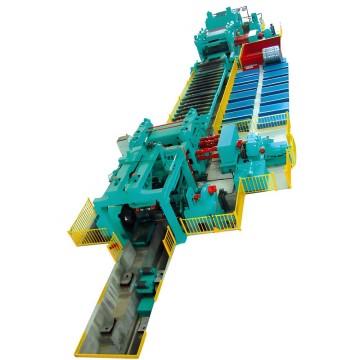
Uncoiling-Leveling-Shearing-Stacking Line
Automated sheet processing powerhouse equipped with hydraulic shearing mechanisms and scratch-free stack collection.
View SpecificationThe Global Industrial Landscape for CRC Slitting Lines
Analyzing the transformation of cold rolled coil (CRC) processing across automotive lightweighting, electrical steel laminations, and consumer durables.
Advanced High-Strength Steels (AHSS)
The global transition toward lightweight vehicle architectures demands slitting machinery capable of slicing DP980, QP1180, and martensitic grades without blade chipping, edge work-hardening, or mechanical twist.
Electrical Steel & EV Traction Motors
Non-oriented (CRNGO) and grain-oriented (CRGO) electrical steels demand strict burr thresholds under 0.01 mm to prevent eddy current losses in core lamination packs, driving ultra-high precision knife arbor dynamics.
Zero-Defect Surface Tolerances
For appliance skins and architectural panels, cold-rolled coils are vulnerable to surface impressions. Modern coil processors require non-marking polyurethane rolls, loop pit dust covers, and tension bridle cushions.
The Engineering Reality of Cold-Rolled Slitting Dynamics
Cold rolled coil (CRC) processing differs significantly from traditional hot-rolled slitting due to work-hardening characteristics, thinner gauges (typically 0.15 mm to 3.2 mm), and sensitive surface finishes. Processing CRC requires high rotational stability of the slitting arbors with radial runout held strictly within ±0.002 mm. A minute deflection in the slitter arbor results in uneven horizontal and vertical knife clearances, generating excessive edge burrs, premature knife wear, and camber defects that cascade into downstream automated punching or roll-forming lines.
Across North America, the European Union, Southeast Asia, and the Middle East, manufacturing enterprises are replacing aging mechanical line setups with high-speed automated CRC slitting systems. These automated lines integrate optical loop controls, robotic slitter knife setup mechanisms, automatic strip tension modulation, and automated packaging lines to maintain high yields and minimal downtime.
Why Global Buyers Procure CRC Slitting Lines from Wuxi, China
Combining vertical manufacturing integration, high-precision machining centers, and deep industrial clusters in the Yangtze River Delta.
Complete In-House Metallurgy Ecosystem
Wuxi Jianfa Machine-Building executes every stage under our 40,000 m² roof: structural stress-relief annealing, heavy gantry milling, CNC arbor boring, hardening, dynamic balancing, and assembly integration.
Tier-1 Component Integration
We combine localized manufacturing cost advantages with globally standardized automation: Siemens S7-1500 PLCs, Parker/Rexroth hydraulic valves, NSK/SKF ultra-precision bearings, and Yaskawa servo drives.
TCO & Capital Efficiency
Delivering European-tier slitting tolerance and speed specifications at 40% to 55% lower initial capital expenditure, drastically shortening the ROI timeframe for international service centers.
Engineering Architecture & Localized Use Cases
Configuring custom cold rolled slitting line configurations to suit unique industrial applications and material standards.
| Application Scenario | Target Material & Yield | Critical Engineering Focus | Line Speed & Capacity |
|---|---|---|---|
| Automotive Stamping Blanks | CR Deep-Draw, DP600/800, σs ≤ 800 MPa | Zero surface scratching, hydraulic dual-shim knife adjustment, camber ≤ 0.5 mm/2m | Up to 220 m/min; 0.3 - 2.5 mm thickness |
| Transformer & Motor Cores | CRNGO, CRGO Silicon Steel, σs ≤ 450 MPa | Tungsten carbide circular blades, burr ≤ 0.01 mm, precision slit width ±0.02 mm | Up to 180 m/min; 0.2 - 0.65 mm thickness |
| Precision Welded Tubes | Q235B, SPCC, SPHC Cold-Reduced Strip | Strip edge conditioning, quick changeover turnstile, pneumatic tension pads | Up to 160 m/min; 0.5 - 3.2 mm thickness |
| Home Appliance Outer Panels | Electro-Galvanized (SECC), Pre-Painted CRC | Polyurethane elastomer rolls, vacuum tension bridle, scrap edge ballers | Up to 200 m/min; 0.4 - 1.6 mm thickness |
Automated Tooling Turnstile & Off-Line Setup
To overcome changeover bottlenecks, Wuxi Jianfa lines feature dual or triple-arm rotating turnstiles. While the running line processes a coil, operators configure the next knife and spacer setup off-line with CNC digital caliper guidance. Line swap-over can be achieved in under 15 minutes, boosting overall equipment effectiveness (OEE) by up to 35%.
Differential Recoiler Mandrel Technology
Due to gauge variations between coil center and edges (crown effect), slit strips recoil at varying diameters. Our lines utilize individual differential friction shafts or advanced pneumatic multi-zone tension separators, preventing loose inner loops and uneven coil telescoping without damaging the cold-rolled surface.
Global Corporate Procurement Checklist for CRC Slitting Equipment
Critical engineering criteria international procurement directors must audit before contracting an industrial slitting line.
1. Arbor Rigidity & Bearing Tolerance
Verify that slitter shafts are forged from 42CrMo or 40Cr alloy, quenched and tempered to HRC 52-55, and supported by super-precision cylindrical roller bearings to prevent high-speed rotational vibration.
2. Strip Surface Protection System
Inspect all strip-contact components: polyurethane entry table rollers, felt/rubber wipe tensioners, air cushion looping plates, and non-metallic guiding arms to safeguard sensitive cold-rolled surfaces from galling.
3. Loop Control Automation
Demand ultrasonic or photoelectric depth feedback across the loop pit. Dual loop architectures guarantee line isolation, keeping uncoiler backlash separate from high-tension recoiling dynamics.
4. Scrap Edge Handling Options
Assess scrap management based on gauge: rotary side scrap choppers with tungsten cutting edges for continuous disposal, or high-speed oscillating winder bobbins for thin, sensitive ribbons.
5. International CE & Safety Compliance
Verify safety light curtains, perimeter interlocking fencing, emergency e-stop pull-cords, hydraulic safety dump circuits, and UL/CE compliant electrical control cabinetry enclosures.
6. Remote Tele-Diagnostics
Industrial PLC architectures equipped with VPN or IoT gateway routers permit Jianfa automation specialists to debug software algorithms, optimize servo tuning, and assist operators globally in real time.
Frequently Asked Questions: CRC Slitting Operations
Direct technical clarifications from Wuxi Jianfa's metallurgical machine-building team.
What coil processing equipment does Wuxi Jianfa manufacture?
How do you eliminate strip camber and edge burrs when slitting high-yield CRC?
Which steel alloys and non-ferrous materials can our lines slit?
How does Wuxi Jianfa support overseas installation, commissioning, and staff training?
What engineering data is required to receive an accurate technical proposal and layout?
Can international buyers inspect equipment and run strip tests prior to shipment?
Explore Our Industrial Coil Processing Machinery
Review our core machinery range built to handle diverse metal alloys, sheet thicknesses, and volume demands.

Flying Shear Production Line
Continuous dynamic shearing line operating at speeds up to 100 m/min with synchronized servo tracking.
View Line Details
Precision Slitting Line
Factory-direct high speed coil rotary slitting system equipped with dual eccentric arbor adjustments.
View Line Details
CE Standard Cut to Length Line
CE-certified high-accuracy leveler and hydraulic shearing cell delivering stacked sheets with tight tolerances.
View Line Details
Heavy-Plate Leveling Machine
Heavy 4-Hi and 6-Hi roll configurations designed to eliminate coil set and cross bow in thick-gauge steel.
View Line Details
Sheet Straightening Machine
Precision multi-roll straightener built to deliver stress-free sheet leveling for laser cutting downstream.
View Line Details
Plate Moving Shear Production Line
Continuous cutting line that shears strips on-the-fly, eliminating surface indentations caused by stop-start cycles.
View Line Details
Stainless Coil Stacking Line
Engineered for stainless steel with protective film application, paper re-winder, and magnetic drop stackers.
View Line Details
CRC Rotary Slitting & Recoiling Line
High-speed slitting system with loop accumulator pit, edge guide servos, and automatic packaging turnstiles.
View Line DetailsRequest an Engineered Line Proposal
Connect directly with Wuxi Jianfa's technical engineering team. Receive comprehensive machine layouts, cycle-time calculations, and transparent FOB/CIF pricing within 24 business hours.
Direct Sales & Technical Support
Factory Base: No. 58 Qunxing Road, Meicun, Xinwu District, Wuxi, Jiangsu, China