
High-Performance Coil Processing Machinery
Configured for diverse steel grades including cold-rolled, hot-rolled, automotive ultra-high-strength steel, electrical steels, and prime surface aluminum alloy coils.
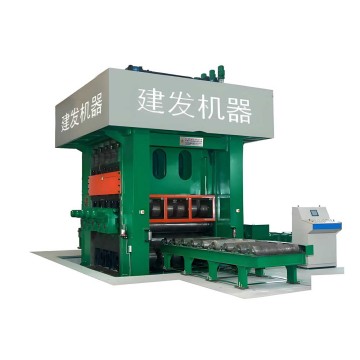
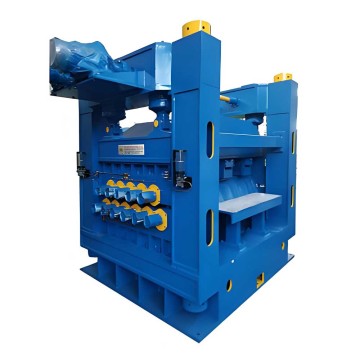
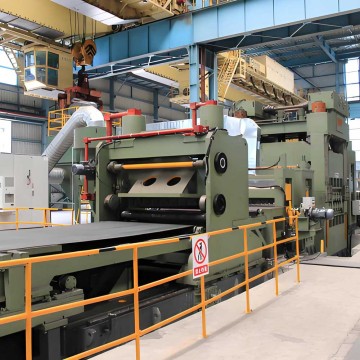
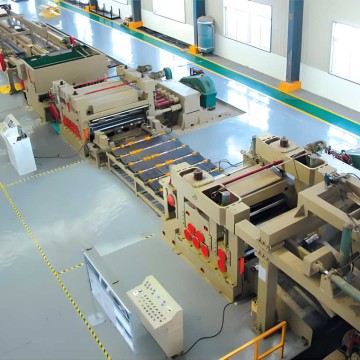
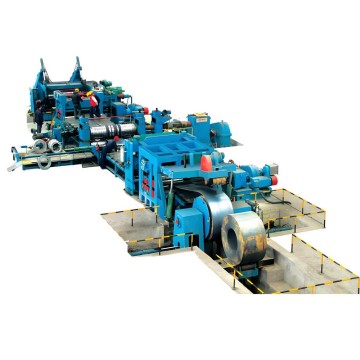
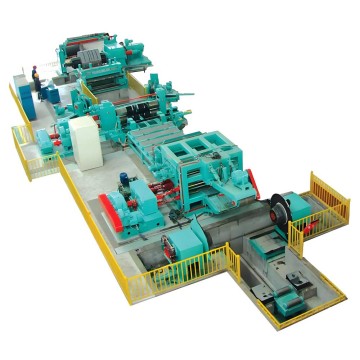
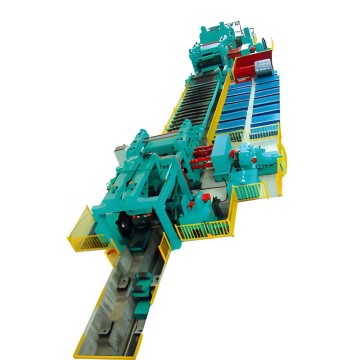
Engineering Anatomy of an Industrial Metal Sheet Slitting Machine
A metal sheet slitting machine is an orchestrated assembly of mechanical rigidity, dynamic drive synchronization, and metallurgical tooling. Micron-scale precision prevents edge burr deformation and excessive knife degradation.
Rotary Arbor Deflection Control
Dual-arbor slitter heads are cast from spheroidal graphite iron and heat-treated to resist thermal and dynamic deformation. Arbors are precision-ground with runouts held under ±0.003 mm, preventing edge camber and uneven shear planes across wide strips.
Dynamic Back-Tension Regulation
Maintains consistent strip tautness across varying slit strands using air-cooled tensioning brakes, pneumatic pad assemblies, or non-marking belt bridles. Eliminates outer lap looseness and internal cinching during tight rewinding.
Hydraulic Turret Tool Loading
Quick-change arbor turrets pre-rig secondary tooling while the primary arbor is operating. Reduces retooling downtime from 45 minutes to under 8 minutes, maximizing overall equipment effectiveness (OEE) for mixed batch orders.
| Engineering Attribute | Standard Steel Slitter | Heavy-Gauge Structural Slitter | High-Speed Thin Precision Slitter |
|---|---|---|---|
| Applicable Thickness Range | 0.5 mm – 3.0 mm | 3.0 mm – 16.0 mm | 0.15 mm – 1.5 mm |
| Material Yield Capacity | ≤ 450 MPa | ≤ 850 MPa (Q355/S355/Strenx) | ≤ 1200 MPa (AHSS / Stainless) |
| Operating Line Velocity | 80 – 120 m/min | 30 – 60 m/min | 150 – 250 m/min |
| Slitting Arbor Runout | ≤ 0.008 mm | ≤ 0.012 mm | ≤ 0.003 mm |
| Burr-to-Thickness Ratio | ≤ 5% to 7% | ≤ 8% to 10% | ≤ 3% to 4% |
Localized Applications of Slitting Equipment
From automotive stamping plants in North America to solar torque tube manufacturing in the Middle East, our coil processing lines adapt to specialized industrial demands.
Automotive Body & Structural Components
Requires flawless surface preservation and strict edge burr thresholds (<3%) on Advanced High-Strength Steels (AHSS) and exposed aluminum panels (6000 series). Minimizes post-shearing micro-cracks during deep-drawing operations.
Solar Mounting & Infrastructure Support
Demands heavy-duty continuous slitting of thick pre-galvanized (Zn-Al-Mg) coils up to 6mm. The tooling setup prevents micro-flaking of the protective zinc coating at the shear interface, maintaining high corrosion resistance in outdoor fields.
Electrical Transformer Core Silicon Steel
Processing grain-oriented (CRGO) and non-oriented electrical steel strips down to 0.20 mm. Tight arbor tolerance control prevents edge burrs that would otherwise short-circuit transformer core laminations and cause magnetic core losses.
Precision Welded Tube & Pipe Mills
Longitudinal slitting lines engineered for continuous strip width tolerances within ±0.05 mm. Consistent strip width is required to achieve stable seam tracking in High-Frequency Induction (HFI) welding operations.
HVAC Ducting & Architectural Cladding
High-volume processing of prepainted and galvanized coil stock. Dual tension control loops prevent surface micro-scratches on exterior-grade paint systems while ensuring uniform recoil densities across multiple narrow strands.
Toll Processing & Steel Service Centers
Demands wide flexibility for varied material grades (mild steel, aluminum, stainless). Equipped with automated arbor changeovers and multi-step shimless tooling tooling recipes managed via industrial HMI recipes.
Chinese Supply Chain Resilience & Wuxi Industrial Ecosystem
Wuxi Jianfa Machine-Building operates at the core of the Yangtze River Delta heavy industrial corridor, providing end-to-end quality control and rapid component turnarounds.
In-House Machining & Quality Rigor
By keeping large boring, surface grinding, thermal treatment, and final line assembly inside our 40,000 m² plant, we retain full control over component lead times, geometric tolerances, and assembly alignment.
Integrated Metallurgical Cluster
Our location in Wuxi provides immediate access to specialty alloy forged steels (such as Cr12MoV, SKD11, high-carbide tool grades) and precision hydraulic valving. This reduces our procurement cycles by up to 45% compared to western equivalents.
Direct Deep-Water Port Access
Located near the Port of Shanghai, heavy structural machinery frames, large-diameter recoiler mandrels, and hydraulic assemblies move from shop-floor test trials onto breakbulk vessels with minimal transit risk.
Global Industry Landscape & Technological Roadmap
The global coil processing sector is transitioning toward Industry 4.0 automation, tighter environmental controls, and low-waste slitting protocols.
AI-Assisted Optical Edge Quality Verification
Transitioning toward real-time high-speed optical scanning positioned downstream of the rotary slitter head. Edge inspection algorithms detect knife wear, micro-burrs, and edge fractures on the fly, alerting operators prior to recoiling.
Automated Robot Tooling Placement
Collaborative multi-axis robotic gantry systems read strip optimization schedules directly from enterprise ERPs. Knife and shim configurations are loaded onto auxiliary arbors automatically, eliminating manual rigging errors.
Regenerative VFD Energy Braking
Modern common DC-bus frequency drives capture mechanical braking energy generated by the uncoiler and bridle drag systems, redirecting excess power to the main recoiler motor to reduce total facility kWh consumption by up to 28%.
Engineering Standards, Safety & Field Support
Our heavy manufacturing adheres to global CE directives, UL/CSA control panel integration, and structured overseas commissioning teams.
International Safety Directives
Designed in compliance with European Machinery Directive 2006/42/EC and EN ISO 13849-1 functional safety. Lines include fail-safe hydraulic interlocks, category-4 perimeter optical curtains, and zoned emergency-stop loops.
On-Site Commissioning by Factory Engineers
We deploy senior mechanical and electrical engineers directly to your plant for foundation alignment, level calibration, hydraulic line purging, cold/hot commissioning, and comprehensive bilingual operator training.
Remote IoT Diagnostics & Tele-Support
Industrial edge VPN modules enable our R&D engineering center in Wuxi to analyze drive performance curves, troubleshoot PLC alarms, and optimize loop control algorithms in real time across any time zone.
Frequently Asked Questions on Metal Sheet Slitting Lines
Detailed technical considerations for engineering managers and plant procurement leads.
What coil processing equipment does Wuxi Jianfa manufacture?
Which materials can your slitting and cut to length lines process?
How do I choose between a slitting line, a cut to length line and a flying shear line?
What causes edge camber during coil slitting, and how do Jianfa lines prevent it?
What information should I send to receive an accurate technical proposal?
Do you support installation, commissioning and operator training overseas?
Can I visit the factory and inspect my equipment before delivery?
How is burr-free slitting achieved on high-strength automotive steels (>980 MPa)?



Industrial Slitting & Cut-to-Length Product Solutions
Examine our full engineering lineup for coils ranging from 0.2 mm to 16 mm in thickness.
Request an Engineering Line Layout & Feasibility Study
Send us your incoming coil parameters (OD/ID, thickness, yield strength) and desired production capacity. A senior Wuxi Jianfa application engineer will generate a complete project layout and cycle-time calculation.