
High-Dynamics Flying Shear Production Systems for Iberian Mills
Engineered for Spanish metal service centers, automotive blanking lines, and solar structural fabricators requiring continuous cutting without stop-and-go inertia defects.



Macro-Industrial Dynamics of Spanish Coil Processing (2025–2030)
Strategic analysis of metallurgical demand, regional production hubs, and the transition toward high-speed flying shear lines in the Iberian Peninsula.
Regional Manufacturing Clusters & Sourcing Demands
Spain stands as the second-largest automotive manufacturer in Europe and a dominant global powerhouse in solar energy structural component fabrication. The Iberian industrial topography is defined by high-density, specialized metallurgical clusters: the Basque Country (País Vasco) with its deep-seated legacy in heavy steelmaking, forging, and tube extrusion (Bilbao, Vitoria-Gasteiz); Catalonia, anchored by automotive assembly (SEAT Martorell) and its extensive tier-1 stamping supply ecosystem; Valencia and Almussafes, serving massive automotive and export metal centers; and Asturias, home to Europe's major heavy plate and primary steel mills.
Historically, Spanish metal service centers (Centros de Distribución y Corte de Acero) operated traditional start-stop Cut-to-Length (CTL) lines. However, the aggressive transition toward lightweight automotive materials (Advanced High Strength Steels like DP600/DP980, complex phase steels, and 5000/6000 series aluminum alloys) alongside utility-scale solar tracker expansion has rendered stop-and-go cutting obsolete. Spanish processors now require continuous, inertia-free cutting to eliminate roll slippage, prevent surface micro-scratches on exposed automotive sheets, and avoid brake-induced strip bucking.
Technical Transition in Spain: The Shift from Stop-to-Cut to Continuous Flying Shear
In traditional CTL lines, accelerating and decelerating heavy strip coils introduces cyclic hydraulic shock and surface friction marks. A modern Flying Shear Production Line matches the linear velocity of the cutting blade precisely with the continuously advancing strip using dynamic servo electronic camming (E-CAM). This elevates line throughput from 35-40 m/min up to 100–120 m/min, delivering a 250% productivity gain while maintaining length tolerances within ±0.3 mm.
Automotive Blanking Precision
Catalonia and Valencia automotive tiers demand class-A surface preservation without shear burrs. Flying shears ensure zero strip hesitation across the measuring roll, preventing indentations on sensitive exposed skin panels.
Class-A Finish / ±0.2 mm AccuracySolar Tracker & ZM Coated Steels
Spain is Europe's ground zero for tracker manufacturers (PVH, Soltec, STI Norland). These structural elements utilize Zinc-Magnesium (ZM) alloy coatings that crack if stressed under abrupt hydraulic clamping, requiring continuous moving-blade shearing.
ZM310 / Magnelis CompatibilityEnergy Cost Optimization
Spanish industrial electricity tariffs necessitate high-efficiency regenerative drive systems. Wuxi Jianfa lines integrate common DC bus systems that recover braking energy during servo motor deceleration cycles.
Up to 32% Energy RecaptureKinematic Architecture: Rotary Flying Shear vs. Eccentric Crank Mechanics
An in-depth technical examination of synchronizing dynamic blade motion with high-speed uncoiled metal strips.
A true flying shear production line operates on the core mechanical premise that the cutting tool must achieve identical horizontal velocity vector ($V_x$) to the strip material ($V_{strip}$) at the exact millisecond of blade penetration. Any velocity mismatch ($\Delta V = V_x - V_{strip} \neq 0$) induces tension or compressive buckling across the leveling rollers, resulting in edge burring, blade chipping, and dimensional distortion.
| Engineering Attribute | Traditional Hydraulic Stop-to-Cut | Reciprocating Crank Flying Shear | Continuous Rotary Drum Flying Shear |
|---|---|---|---|
| Maximum Line Velocity | 25 – 40 m/min | 60 – 80 m/min | 100 – 120 m/min |
| Strip Surface Contact | Intermittent clamping (friction risk) | Synchronized dynamic clamping | Continuous zero-contact fly-through |
| Length Accuracy (at 80 m/min) | ±0.50 mm / meter | ±0.30 mm / meter | ±0.15 mm / meter |
| Blade Duty Cycle Life | 300,000 cuts before regrind | 650,000 cuts before regrind | 1,200,000+ cuts (Cr12MoV / H13) |
| Leveling Residual Stress | High (re-induced by braking) | Negligible | Completely stress-relieved (6-Hi) |
| Applicable Spanish Industries | General construction rebar/beams | HVAC, metal framing, solar struts | Automotive Class-A, High-Yield Plate |
Multi-Roll Precision Leveling: Eliminating Elastic Memory
High-yield-strength coils processed in Spain, such as S355MC, S500MC, and S700MC, possess extreme residual stresses resulting from hot-rolling cooling gradients. When slit or cut, these internal stresses release, manifesting as crossbow, center buckle, or edge camber. Wuxi Jianfa equips its flying shear lines with high-rigidity 4-Hi and 6-Hi precision cassette levelers.
By subjecting the strip to alternating cyclic plastic-elastic bending through small-diameter, closely spaced work rolls backed by motorized intermediate and back-up rolls, residual stress is homogenized across the full cross-section. The cassette system allows Spanish operators to swap roll sets in under 15 minutes when transitioning between carbon steel and surface-sensitive stainless steel or aluminum.
Strategic Sourcing for Spanish Plant Directors: CAPEX vs. TCO
Comparing German/Italian engineering premiums against Wuxi Jianfa's factory-direct metallurgical integration.
Procurement managers in Bilbao, Barcelona, and Madrid frequently weigh the investment between European equipment integrators (Fagor Arrasate, Salico, Dimeco) and factory-direct Chinese manufacturers. While European machinery offers geographical proximity, it typically carries a 150% to 220% CAPEX premium and lead times extending to 14–18 months.
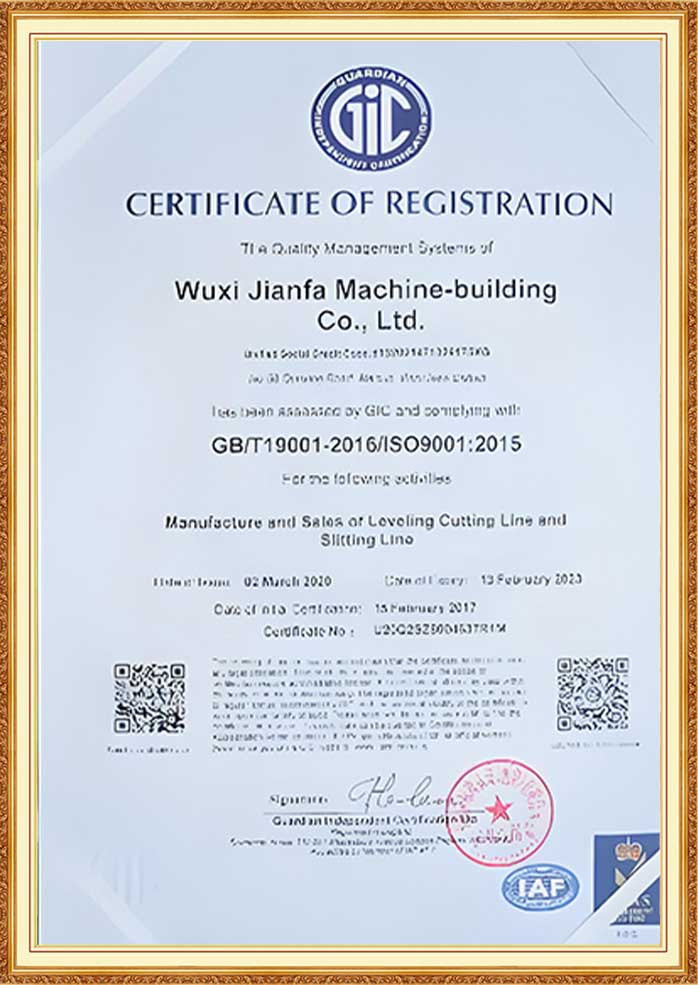
Wuxi Jianfa bridges this paradigm. As a factory-direct manufacturer with a 40,000 m² machining and assembly facility in Wuxi, China, our machines integrate tier-1 global standard components: Siemens S7-1500 PLC & Sinamics S120 dynamic servo drives, Rexroth hydraulics, Schneider low-voltage switchgear, and SKF/NSK heavy spherical bearings. The mechanical steel structures, bed castings, leveling rolls, and eccentric drive shafts are forged, heat-treated, and precision-machined in-house under strict ISO 9001 and CE execution protocols.
The Total Cost of Ownership (TCO) Advantage for Spanish Buyers
By securing a direct factory contract with Wuxi Jianfa, Iberian metal service centers amortize their initial machinery capital within 18–24 months versus 5+ years for European-built equivalents. Spare parts—such as customized H13/Cr12MoV flying shear blades, polyurethane nip rolls, and encoder assemblies—are standardized on open-architecture global hardware, liberating plants from proprietary, overpriced OEM vendor lock-in.
Tier-1 European Components
Standardized on Siemens motion control, Rexroth proportional valves, and Schneider electrics, ensuring local maintenance engineers in Spain have immediate domestic access to spares.
100% Non-Proprietary SparesRapid Delivery to Bilbao / Valencia
Factory fabrication cycles within 120–150 days. Direct sea freight routes from Shanghai to the Port of Valencia, Barcelona, or Bilbao guarantee streamlined customs and arrival.
120-Day Build CycleTurnkey Commissioning & FAT
Full-scale Factory Acceptance Testing (FAT) with client coils in Wuxi before sea packaging. Onsite commissioning engineers dispatched across Spain for installation and operator training.
Full Pre-Shipment Live TestingSpanish Industrial Compliance: UNE-EN 13985 & CE Machinery Directive
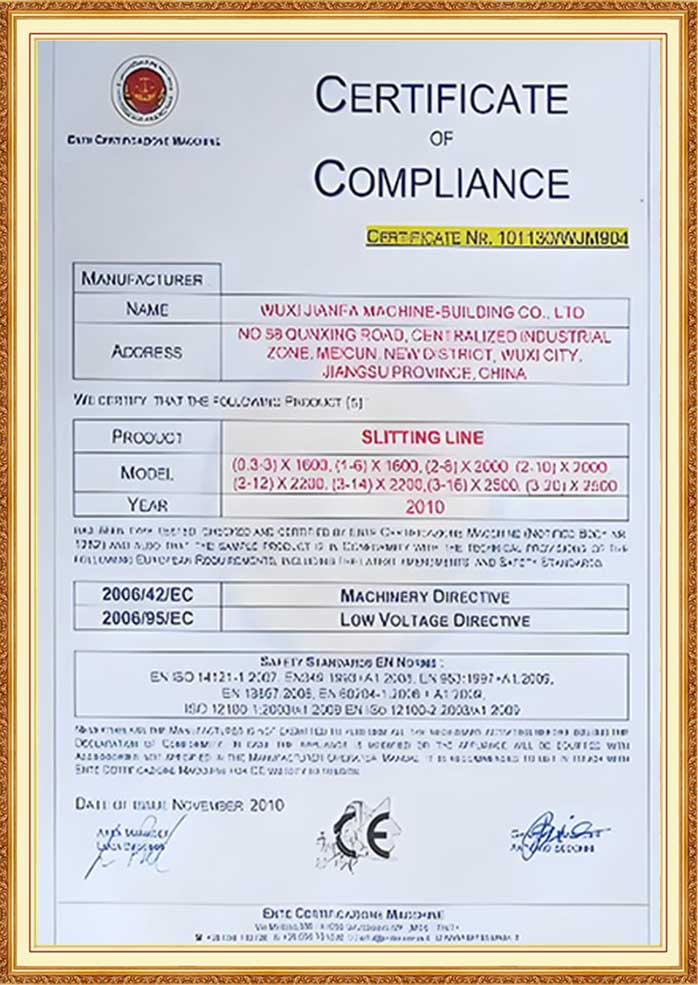
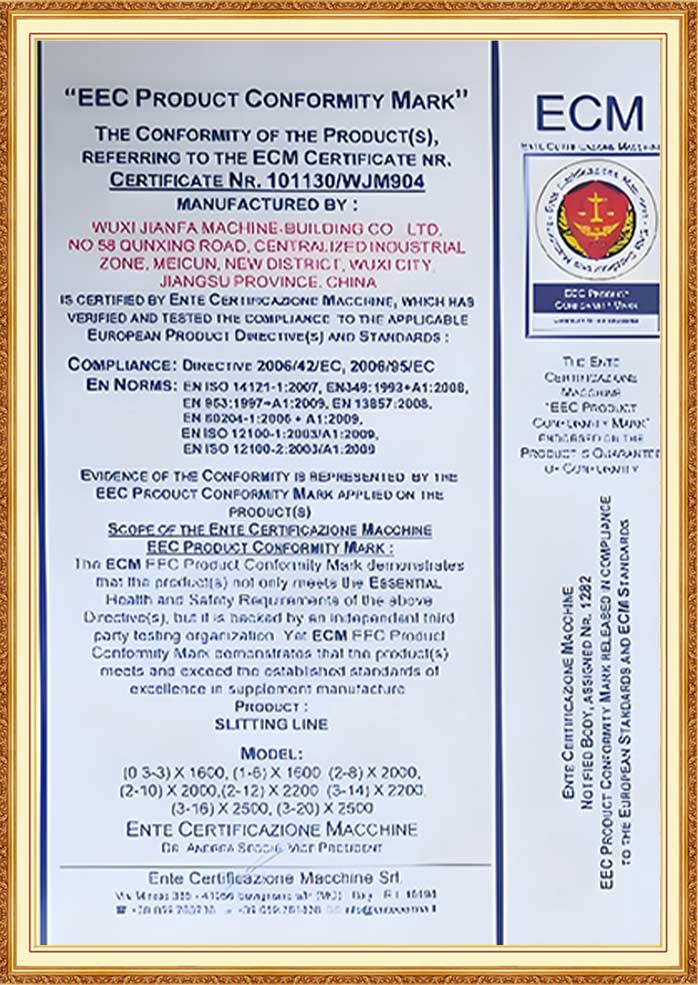
Eliminating regulatory hurdles through comprehensive third-party notified body certifications and safety documentation.
Deploying heavy metallurgical machinery in Spain requires stringent conformity with European and Spanish national occupational safety regulations. Under the Spanish Real Decreto 1215/1997 and the harmonized European Machinery Directive 2006/42/EC, equipment must undergo rigorous risk assessments and conformity verification.
Our flying shear and coil processing production lines are built strictly adhering to:
- UNE-EN 13985 (Machine tools - Safety - Guillotine shears): Mandating optical safety curtains, interlocking mechanical interlocks, and fail-safe hydraulic circuits during high-speed shearing operations.
- UNE-EN ISO 13849-1 (Safety of machinery - Safety-related parts of control systems): Engineered with dual-channel emergency stop circuits achieving Performance Level 'd' and 'e' (PL d/e).
- Low Voltage Directive 2014/35/EU & EMC Directive 2014/30/EU: Shielded dynamic servo motor cabling and high-grade harmonic filtration ensuring zero electromagnetic interference with surrounding plant robotics.
Verified Factory Certifications & ISO Qualifications
Documented metallurgy standards verifiable through national and international accrediting bodies.
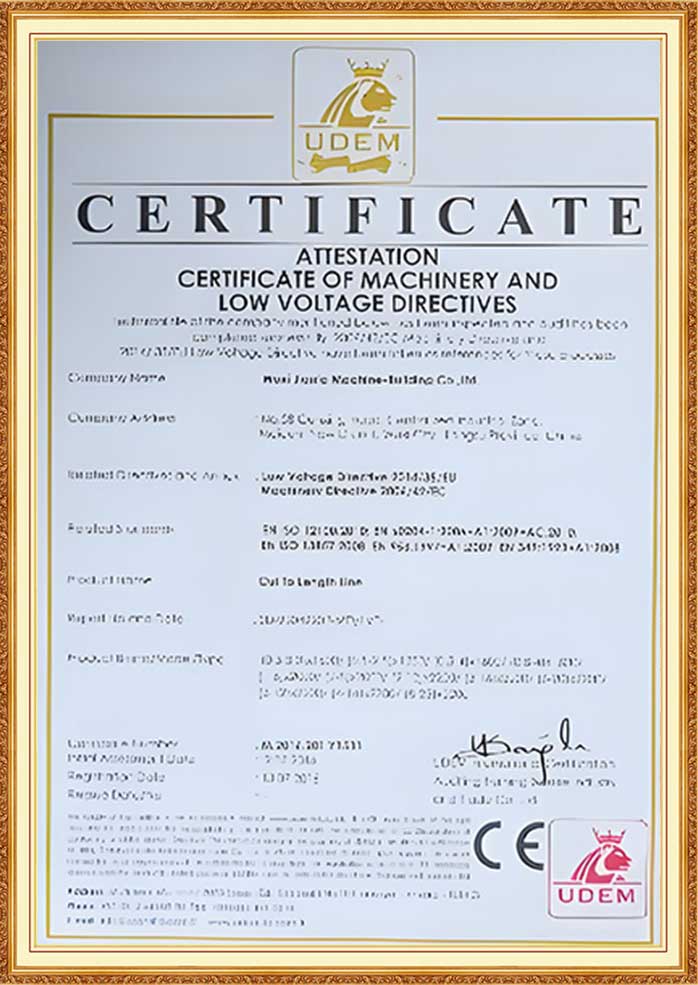 ISO 9001:2015 QC
 CE Conformity Mark
 National Metallurgy Honor
 Enterprise License
 Design Patent Registry
 Heavy Engineering Credit
Technological Roadmap (2025–2030): AI Automation & Closed-Loop Quality
How intelligent sensor integration and remote IoT diagnostics empower autonomous coil cutting operations.
Laser Triangulation Flatness Inspection
Online multi-point laser scanners map surface planarity post-leveler. The system auto-adjusts motorized intermediate backup roll penetration in real-time to neutralize edge waves.
Closed-Loop Auto FlatteningMotorized Precision Blade Gap Auto-Setting
When changing material recipes from 1.5 mm stainless steel to 6.0 mm S355 structural steel, the shear automatically adjusts horizontal blade clearances via high-resolution servo jacks in seconds.
< 10 Second Recipe ChangeIberian Remote Cloud Telemetry (VPN)
Integrated VPN routers provide encrypted remote monitoring from Wuxi to Spanish factories, facilitating real-time cycle profiling, predictive bearing maintenance, and instant troubleshooting.
24/7 Remote DiagnosticsTurnkey Metal Coil Processing Portfolio for Spanish Distribution Centers
Direct manufacturer solutions covering high-strength plate leveling, continuous flying shears, precision slitting, and automated magnetic stacking.








Frequently Asked Questions by Iberian Plant Directors
Detailed engineering, logistical, and warranty answers compiled by Wuxi Jianfa's technical sales team.
What cutting tolerance can be maintained when operating a flying shear at 100 m/min?
Can the same flying shear line process both high-tensile steel (S700MC) and surface-sensitive aluminum?
How does Wuxi Jianfa guarantee CE certification and conformity with Spanish RD 1215/1997?
What is the typical shipping timeline and logistics route from Wuxi to Spanish ports?
How is on-site installation, commissioning, and staff training handled in Spain?
Upgrade Your Plant's Output with Wuxi Jianfa
Submit your coil specifications, yield strength parameters, and plant footprint. Our senior technical team will generate a comprehensive line configuration proposal, kinematic calculation sheet, and ROI analysis within 24 hours.