
High-Performance Cut-to-Length & Shearing Equipment
Engineered for high tensile strength processing, optical-grade surface finish, and exact edge tolerances meeting Northern German engineering benchmarks.
-

CE Certification Manufacturer Of Cut to Length Line Hamburg Standard
Explore Specification -

High-Quality Professional Flying Shear Production Line Hamburg Grade
Explore Specification -

Precision Slitting Line Equipment For Hamburg Steel Service Hubs
Explore Specification -
Heavy-Gauge Automatic Cut to Length Line Hamburg Industrial Series
Explore Specification
The Hamburg Coil Processing Landscape & Maritime Synergy
An in-depth perspective on why Hamburg stands as the premier gateway for advanced flat-rolled steel consumption and distribution across Northern Europe.
Port of Hamburg Transshipment Edge
As Germany’s largest seaport, the Port of Hamburg operates as a primary intermodal corridor for incoming coils. Modern steel service centers (Stahl-Service-Center) located around Billbrook, Harburg, and Altenwerder demand cut-to-length systems capable of continuous cycle operation directly from dockside railheads to sheet distribution racks.
Aviation & Specialized Shipbuilding
From Airbus operations in Finkenwerder to maritime shipyards along the Elbe, manufacturing in Hamburg requires surface-defect-free cutting of high-strength alloys, architectural stainless steels, and naval-grade carbon steels. Cut-to-length machinery must guarantee absolute squareness (DIN EN 10131 / EN 10051) and eliminate residual stresses.
Shift Towards Green Steel & Decarbonization
With North German industries piloting hydrogen-based direct reduction steelmaking, fabricators are processing newer micro-alloyed, ultra-high-strength steel grades (AHSS/UHSS). These materials exhibit severe springback and extreme yield strengths, requiring robust 6-high levelers with intelligent backup roll cassette management.
Macro Engineering Solutions for Hamburg Metal Processors
Solving complex metallurgy issues: internal stress relief, camber correction, and rapid coil-change automation for maximum plant ROI.
Hydraulic 6-High Levelers
Equipped with intermediate rolls and multi-point micro-adjustable backup shafts. Corrects center buckles, edge waves, and twist while safeguarding delicate galvanized or pre-painted coil surfaces from work roll marking.
Dynamic Rotary & Flying Shears
Engineered for high-volume fabrication plants in Northern Germany. High-speed electronic cam-driven flying shears eliminate the start-stop bottleneck, cutting up to 120 sheets per minute without surface friction or burr creation.
Automated Stacking & Palletizing
Bomb-bay, electromagnetic, and vacuum-cushioned drop stackers protect sheet finishes (stainless steel, mirror-polished aluminum) while automatically banding and weighing pallets for downstream transit to logistics terminals.
Siemens S7-1500 / Profinet CNC
Turnkey Industry 4.0 integration. Features recipe-driven automatic roll positioning, dynamic thickness measurement, real-time energy monitoring, and remote telemetry interface for preventive maintenance protocols.
| System Configuration Parameter | Light Gauge / High Precision Line | Standard Steel Service Center Line | Heavy Plate Flying Shear Line |
|---|---|---|---|
| Strip Thickness Capability | 0.3 mm – 3.0 mm | 1.5 mm – 8.0 mm | 6.0 mm – 25.0 mm |
| Usable Coil Width | 800 mm – 1650 mm | 1000 mm – 2000 mm | 1200 mm – 2500 mm |
| Material Yield Strength | Up to 550 MPa (Stainless/Alu/GI) | Up to 750 MPa (Carbon/Cold Rolled) | Up to 1200 MPa (AHSS / Wear Plate) |
| Leveler Architecture | 6-High (19 or 21 rolls, 40-60mm dia) | 4-High / 6-High (15 to 19 rolls) | 4-High Heavy Cassette (11 to 13 rolls) |
| Cutting Mechanism | Direct Servo Rotary / Crank Shear | Hydraulic Swing / Guillotine Shear | Synchronized Moving / Flying Hydraulic Shear |
| Length Tolerance Accuracy | ±0.15 mm @ 2000 mm sheet length | ±0.25 mm @ 2000 mm sheet length | ±0.50 mm @ 6000 mm plate length |
| Industrial Output Speed | Up to 80 - 100 m/min | Up to 40 - 60 m/min | Up to 30 - 45 m/min continuous |
European Compliance, Delivery Protocols & Lifecycle Support
Bridging Chinese heavy manufacturing efficiency with rigorous German CE and safety regulations for seamless commissioning in Hamburg.
European Machinery Directives (CE)
Every Cut to Length and Slitting Line manufactured for the European Union undergoes extensive conformity assessment: Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and EMC Directive 2014/30/EU. Lines integrate category-4 safety light curtains, interlocking fences, and dual-circuit emergency stops.
Port of Hamburg Direct Logistical Route
Located in Wuxi near the deepwater ports of Shanghai and Taicang, Jianfa prepares seaworthy, corrosion-inhibited packaging with specialized desiccant barriers. Machinery arrives directly at Hamburg (HHLA Container Terminals / Hansaport), eliminating inland transit overheads across intermediate European borders.
Installation, Remote Diagnostics & Spares
Our dedicated European installation engineers manage foundation verification, precision mechanical alignment, hydraulic calibration, and operator trial runs. Remote VPN modules in every control cabinet allow our Chinese R&D center to provide instant PLC parameter optimizations.
Equipping Your Hamburg Facility with Tailored Precision
Provide your coil dimensions, material yield strength, and target production volume. Our senior engineering team will calculate roll deflections and deliver a detailed commercial proposal within 24 hours.
Industrial Cut to Length & Coil Processing Systems
Explore our complete manufacturing series, engineered to handle light gauge, automotive-grade stainless, and heavy structural hot-rolled coils.
-
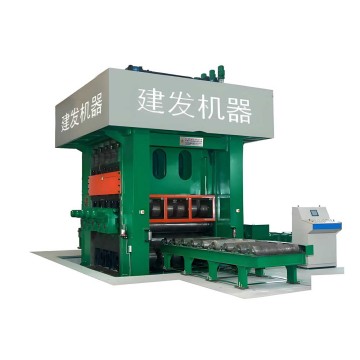
High Strength Leveling Machine Hamburg Heavy Industries Series
View Line Details -
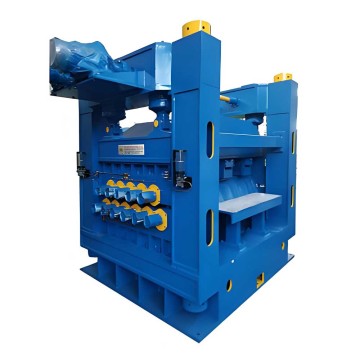
Professional Straightening Machine Hamburg Fabricators Specification
View Line Details -
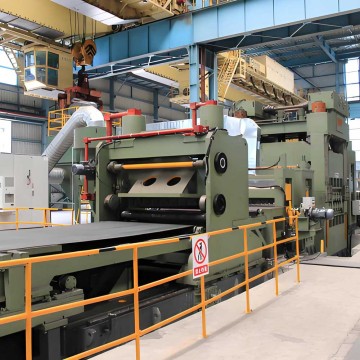
Hot Rolled Plate Moving Shear Line Hamburg Maritime Terminal Model
View Line Details -
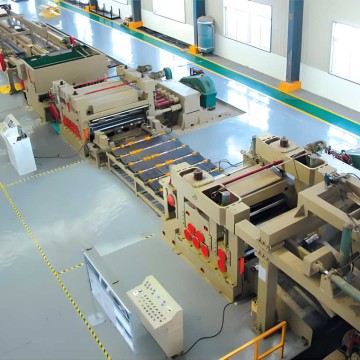
Stainless Steel Uncoiling-Leveling-Shearing-Stacking Line Hamburg Series
View Line Details -
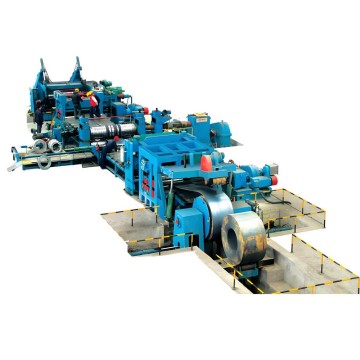
HR Coil Uncoiling-Slitting-Leveling-Cut-To-Length Line Hamburg Edition
View Line Details -
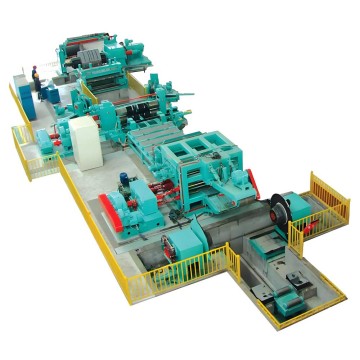
Hot Rolled Sheet Uncoiling, Slitting & Recoiling Line Hamburg Custom
View Line Details -
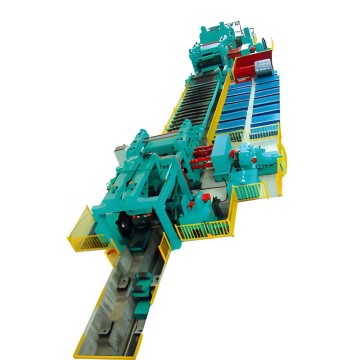
High-Efficiency HR Uncoiling-Slitting-Recoiling Line Hamburg Standard
View Line Details -
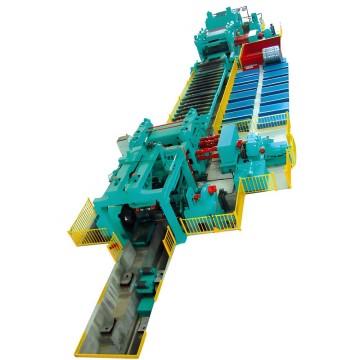
HR Sheet Uncoiling-Leveling-Shearing-Stacking Line Hamburg Model
View Line Details
Frequently Asked Engineering & Procurement Inquiries
Expert answers addressing the real concerns of German plant managers, plant engineers, and metallurgical buyers.
How does your leveling technology manage internal stress in high-strength coils?
Our levelers employ multi-roll configurations (19 to 23 rolls) paired with individually adjustable intermediate and backup support rows. By subjecting the material to alternating plastic bending cycles that diminish in amplitude toward the exit, we achieve up to 85% plastic deformation in outer fibers. This neutralizes cross bow, coil set, and residual stresses, preventing post-cut edge distortion during laser processing.
What is the advantage of choosing a Flying Shear over a Stop-and-Go Guillotine Line?
A stop-and-go cut-to-length line halts strip movement during each shear stroke, creating acceleration-deceleration cycles that can cause surface friction on sensitive metals and cap line output at 30-40 m/min. In contrast, a flying shear synchronizes the blade carrier's linear speed with the continuous strip speed, enabling non-stop shearing at speeds up to 100 m/min with length tolerances held under ±0.2 mm.
Are components easily replaceable and serviceable within the German market?
Yes. All critical electrical and hydraulic sub-assemblies are built with globally available industrial hardware: Siemens S7-1500 PLC control, Rexroth / Parker proportional hydraulic valves, SKF / NSK bearings, and Schneider electrical switchgear. German maintenance teams can source consumables locally without long overseas transit delays.
How are surface marks prevented when processing automotive-grade aluminum & stainless?
For sensitive surfaces, we integrate 6-high roll configurations where intermediate rolls isolate work rolls from backup roll wear. We employ hardened alloy rolls (60-62 HRC, hard chrome or tungsten carbide treated), polyurethane-coated pinch rollers, contactless air-cushion float belts, and vacuum or overhead magnetic stackers to eliminate friction scratches entirely.
What is the typical manufacturing, shipping, and setup timeframe for Hamburg buyers?
Standard manufacturing requires approximately 90 to 120 calendar days depending on automation level and cassette options. Maritime transit from Shanghai to the Port of Hamburg averages 30 to 35 days. On-site positioning, leveling, wiring, and commissioning by our mechanical and electrical engineers take 3 to 4 weeks under ordinary workshop conditions.
Can European clients perform pre-shipment Factory Acceptance Tests (FAT)?
Definitely. We invite client engineers to our 40,000 m² Wuxi production facility (easily reachable from Shanghai) to witness full-load dry runs and coil testing. Alternatively, we provide full digital FAT protocols using HD video streaming, roll hardness verification certificates, laser alignment logs, and sensor performance audits prior to packaging.